Address
Building A1, Runteng Industrial Park, No. 4 Xishan Road, Longteng Community, Shiyan Subdistrict, Bao'an District, Shenzhen 518000, China
Work Hours
Monday to Saturday: 09:00 – 23:00 (UTC+8)
Sunday: closed
Address
Building A1, Runteng Industrial Park, No. 4 Xishan Road, Longteng Community, Shiyan Subdistrict, Bao'an District, Shenzhen 518000, China
Work Hours
Monday to Saturday: 09:00 – 23:00 (UTC+8)
Sunday: closed

Forty answers on the JHIMS DPS-2 automatic SMT lens vibratory feeder — capacity, rejection, machine compatibility, lens range, tooling, cleanroom and ESD configuration, commercial terms, and how to run a sample test on your own lenses.
Before requesting a quotation or sample test, prepare these eight details — they let JHIMS engineering give you a firm answer on compatibility, speed, and price in one round:
Having those eight details ready is the difference between a quotation and a conversation. Lens diameter and geometry decide tooling; material and coating decide whether ESD-safe handling is required; required placement tolerance and target UPH decide the number of channels.
Sent together with the machine model, they let JHIMS engineering answer compatibility, speed and price in one round instead of several. If some figures are still open — most often the exact UPH the line must hit — say so and send lenses instead: the free 48-hour test with 500–800 lenses resolves speed and rejection empirically, and the measured numbers become the acceptance criteria in the order.
This FAQ is part of the JHIMS SMT lens feeding knowledge cluster:
The cluster is organized by the decision you are facing rather than by product code. Start with the product overview if you are still defining the requirement; read the dual-frequency comparison if you are weighing feeding architectures or replacing a feeder that drifts; use the manual versus automatic ROI guide when the question is whether feeding pays for itself at your volume.
Open the troubleshooting guide when a machine is already running on the line, and keep the glossary open while reading a specification sheet, because terms such as amplitude, resonance and escapement carry a precise meaning in feeding. Each page links back here, so the 40 answers below are the shared reference for the whole cluster.
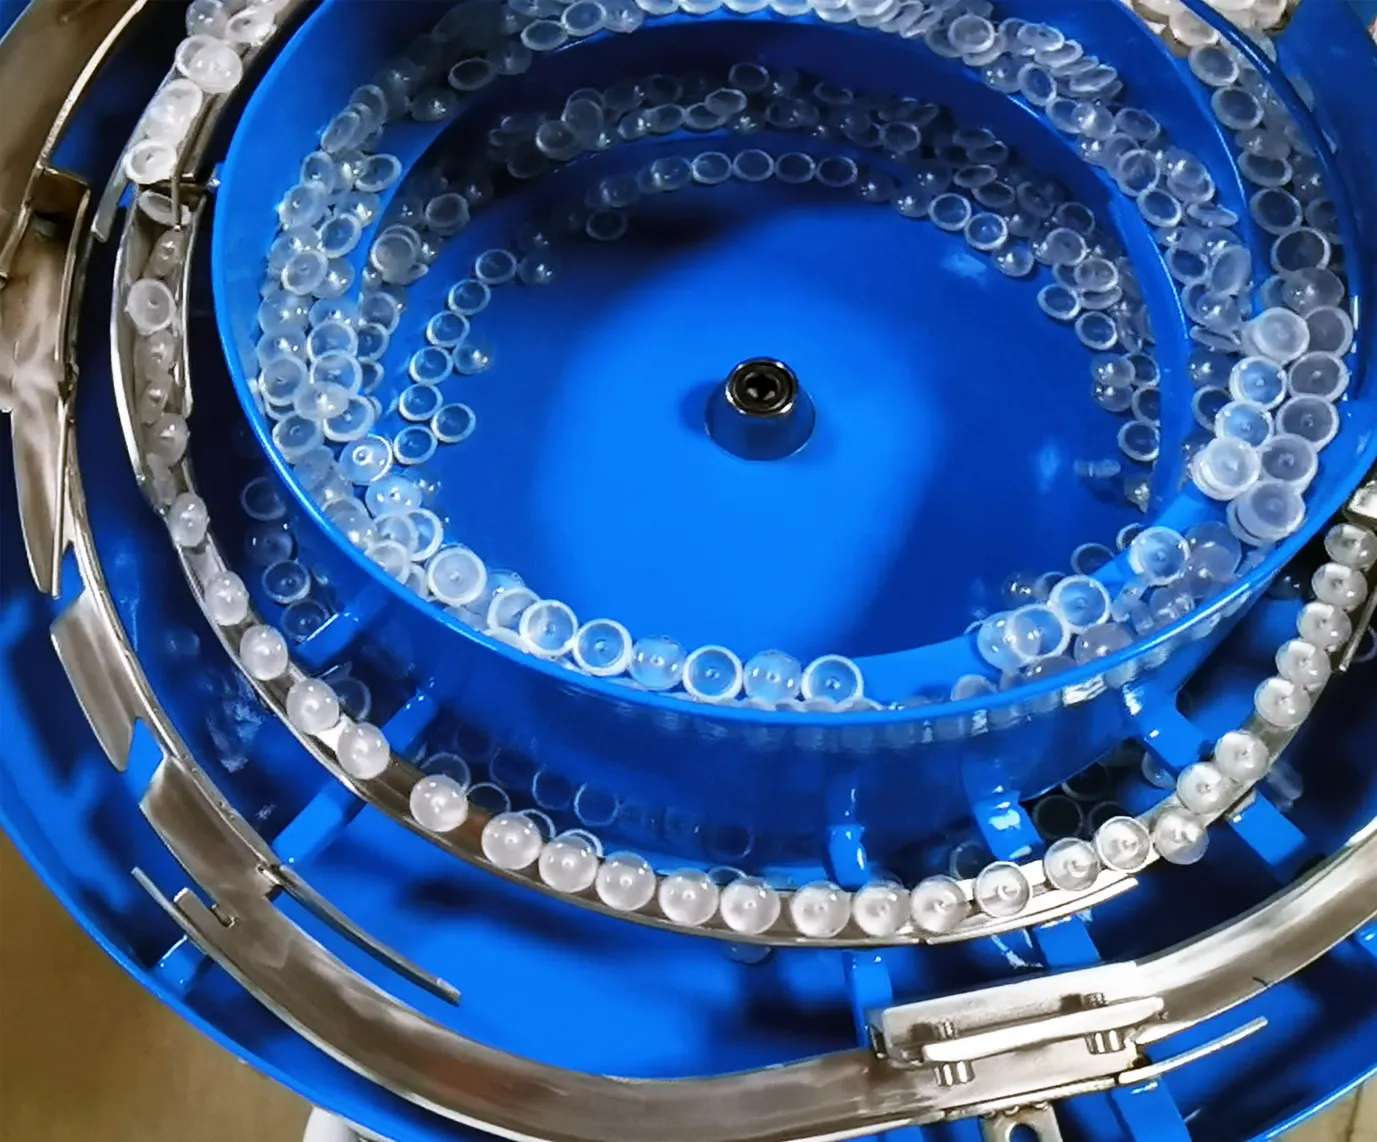
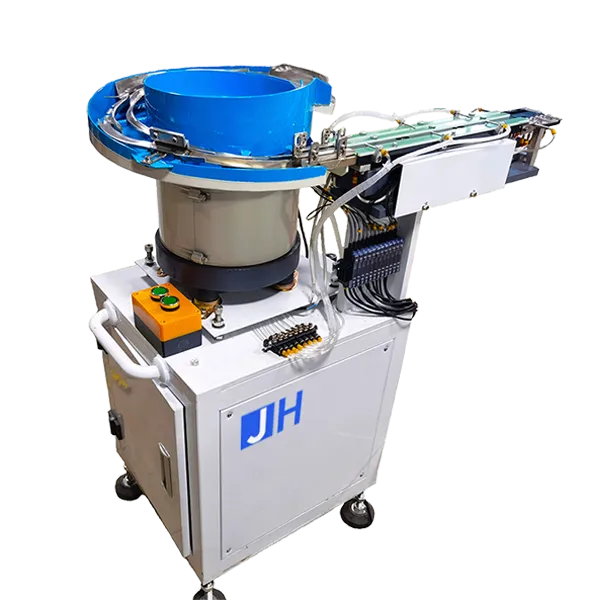
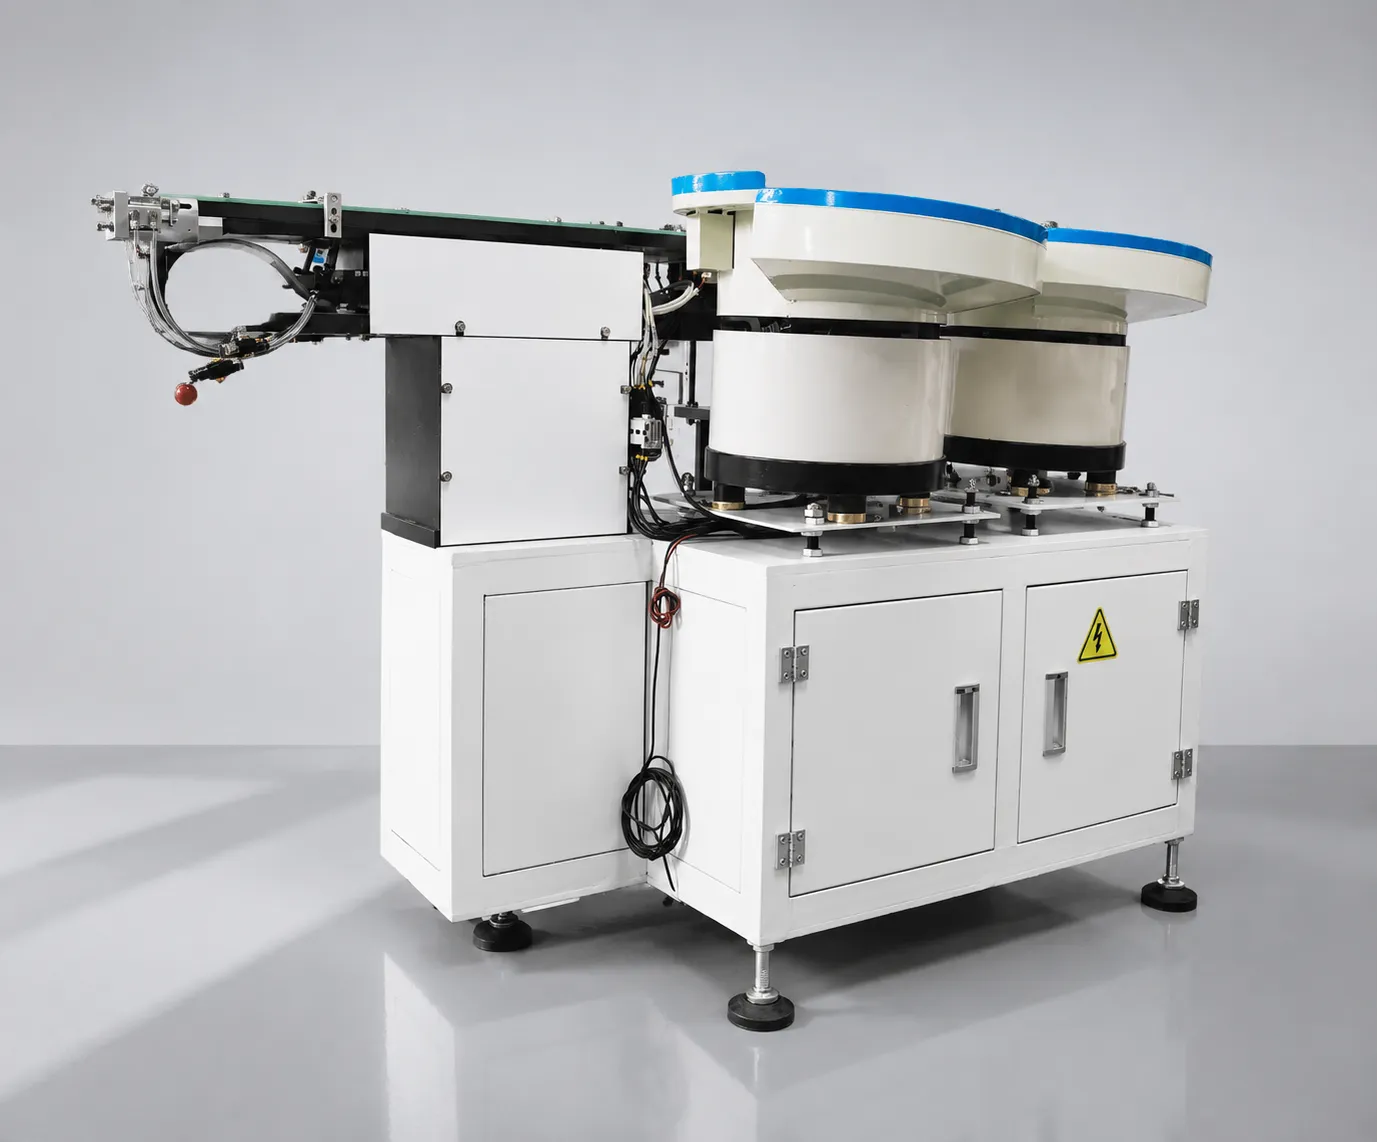
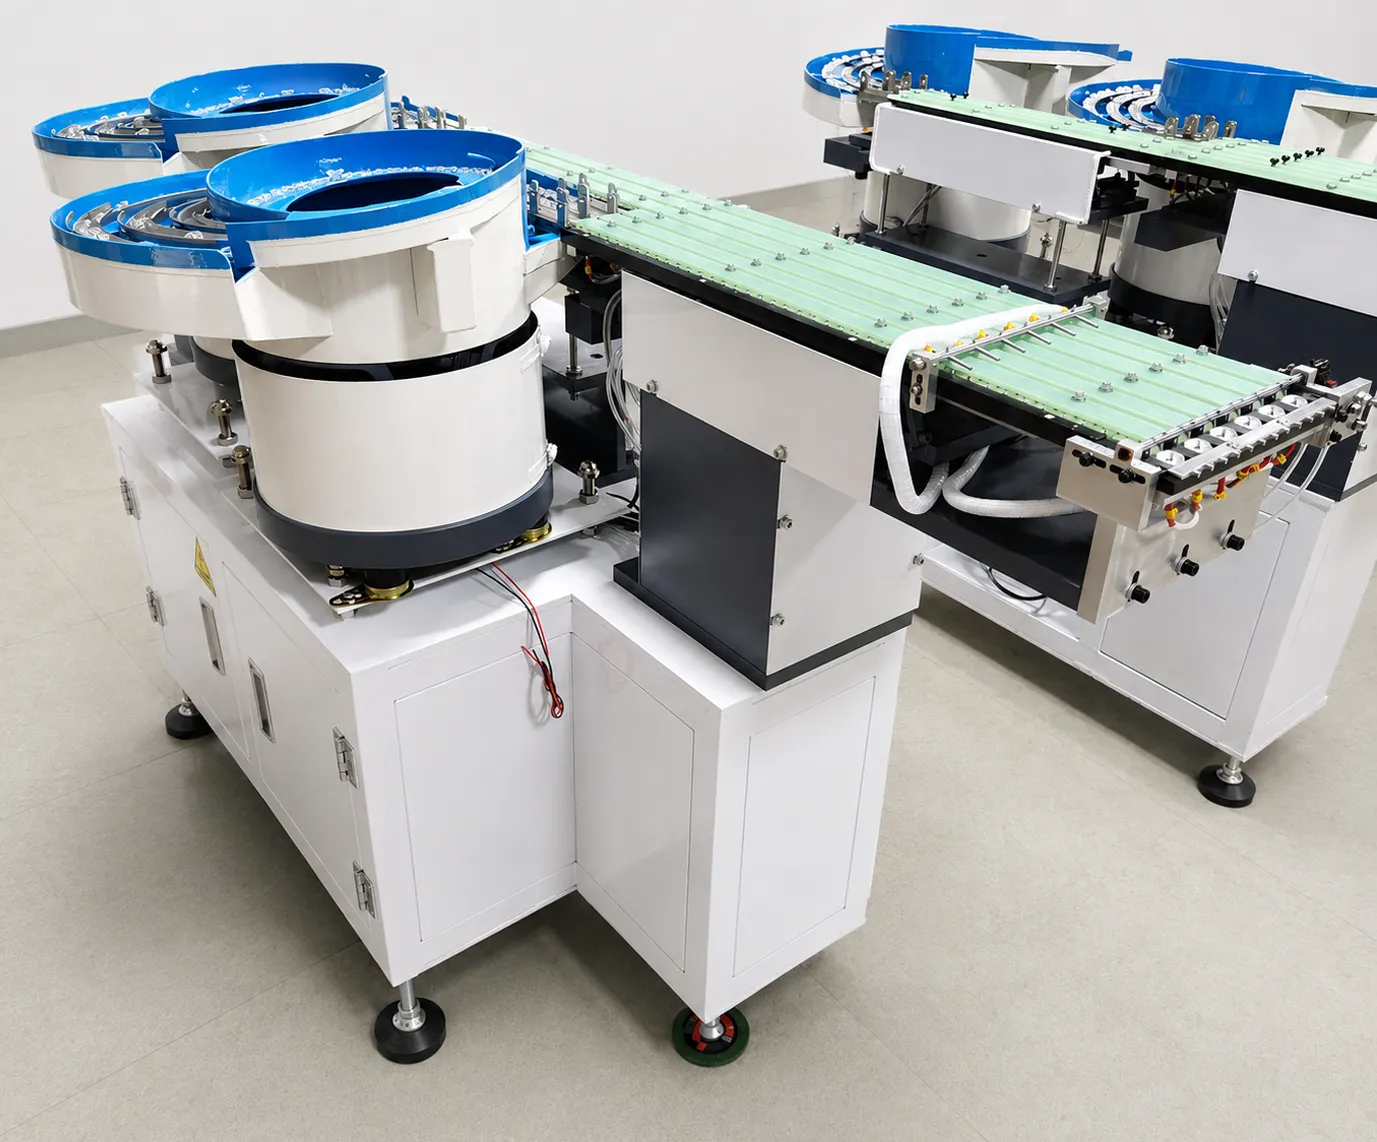
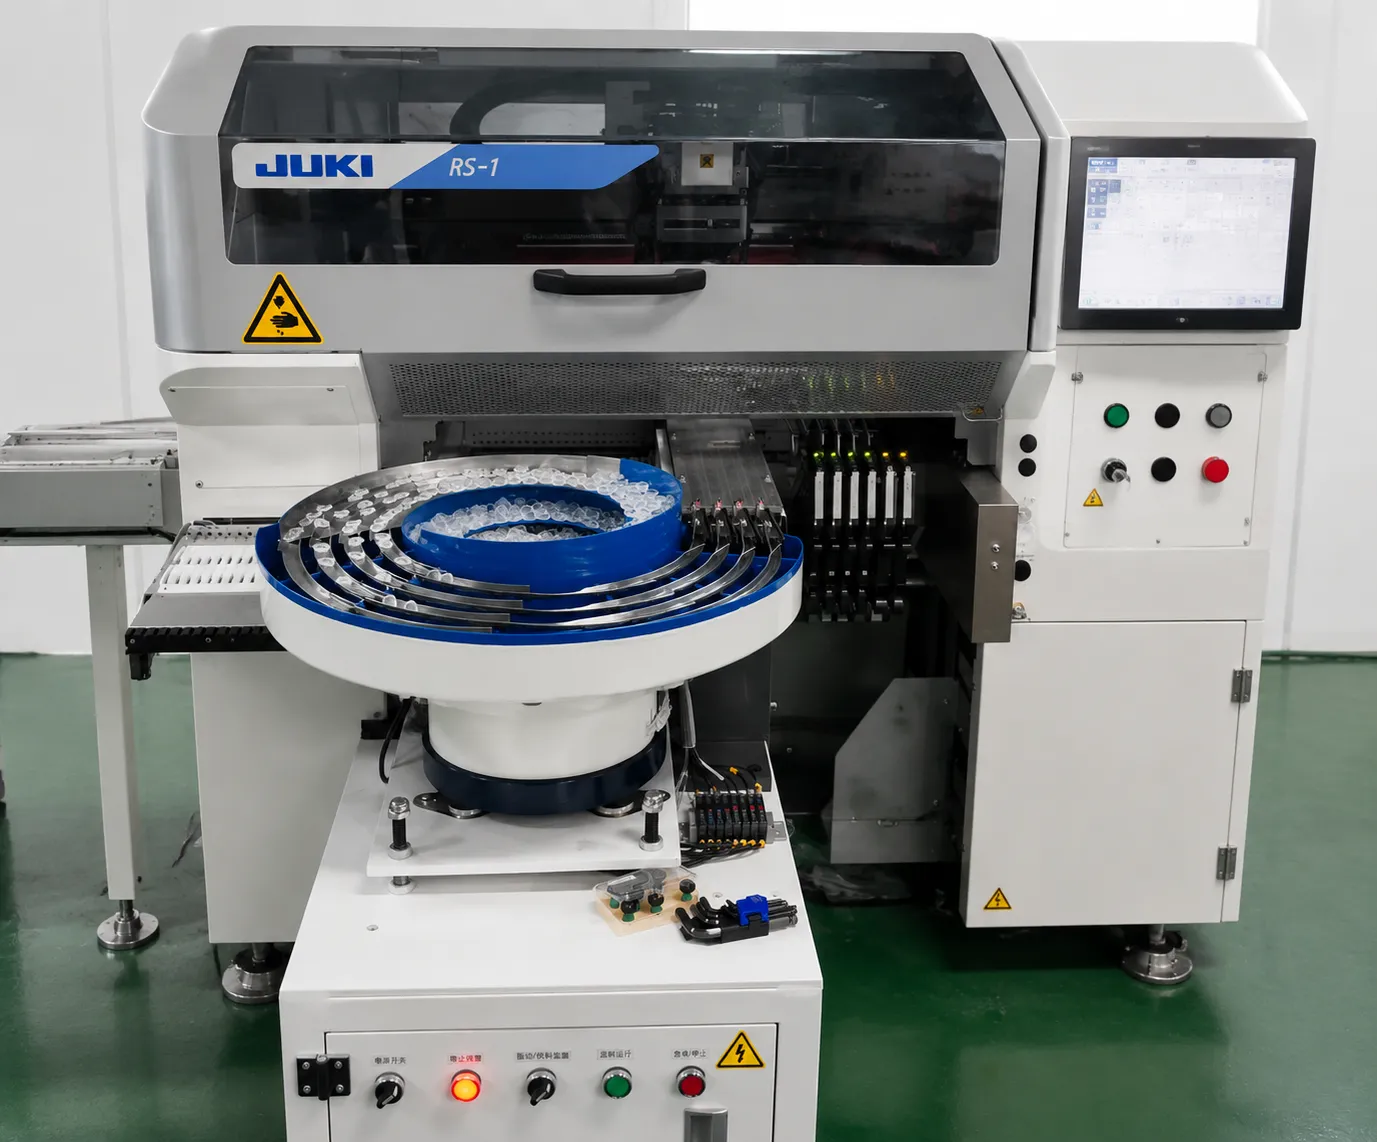
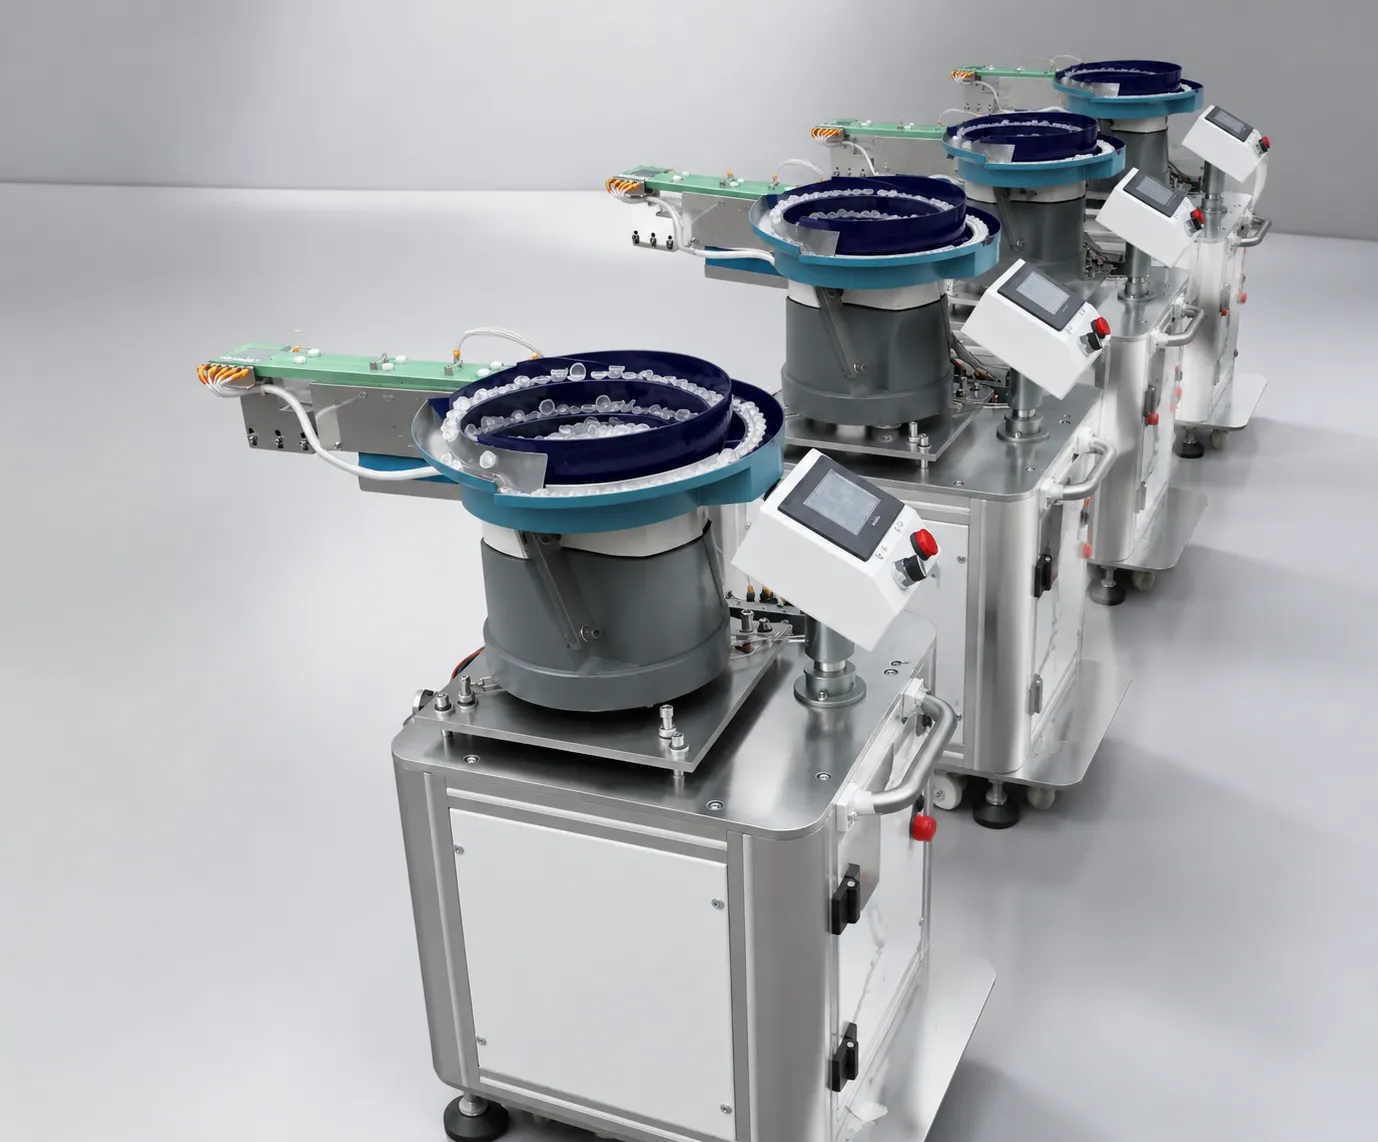
The DPS-2 is an automatic multi-channel vibratory feeder that presents bare optical lenses to the nozzle of a pick-and-place machine, replacing the operator who would otherwise pick each lens by hand. A standard machine carries three to six independent channels, custom builds up to ten, and every channel has its own drive, sensors and jog control.
Throughput is 0.5–1 second per lens per channel — 3,600–7,200 UPH per channel, 14,400–28,800 UPH on a four-channel machine — measured with rejection below 0.5% and typically 0.2–0.4% once tooling is optimized. Control is a Mitsubishi FX5U-32MT/ES PLC with a 7-inch Weintek HMI holding up to 50 lens profiles (Siemens S7-1200 and Pro-face alternative), SMC pneumatics, Keyence sensing and Modbus TCP reporting to MES.
Mechanically the machine is 1050 × 700 × 750 mm at roughly 130 kg, runs on single-phase 220 V AC at 0.55 kVA rated, needs 0.4–0.6 MPa compressed air and produces under 65 dB(A) at one meter — standard industrial floor loading, no special foundation.
For ESD-audited lines the bowl carries a conductive coating of 10⁶–10⁹ Ω per IEC 61340-5-1 and the track inserts are static-dissipative; for cleanroom work an ISO Class 7 configuration is available with sealed bearings, low-outgassing materials and a HEPA-filtered cabinet.
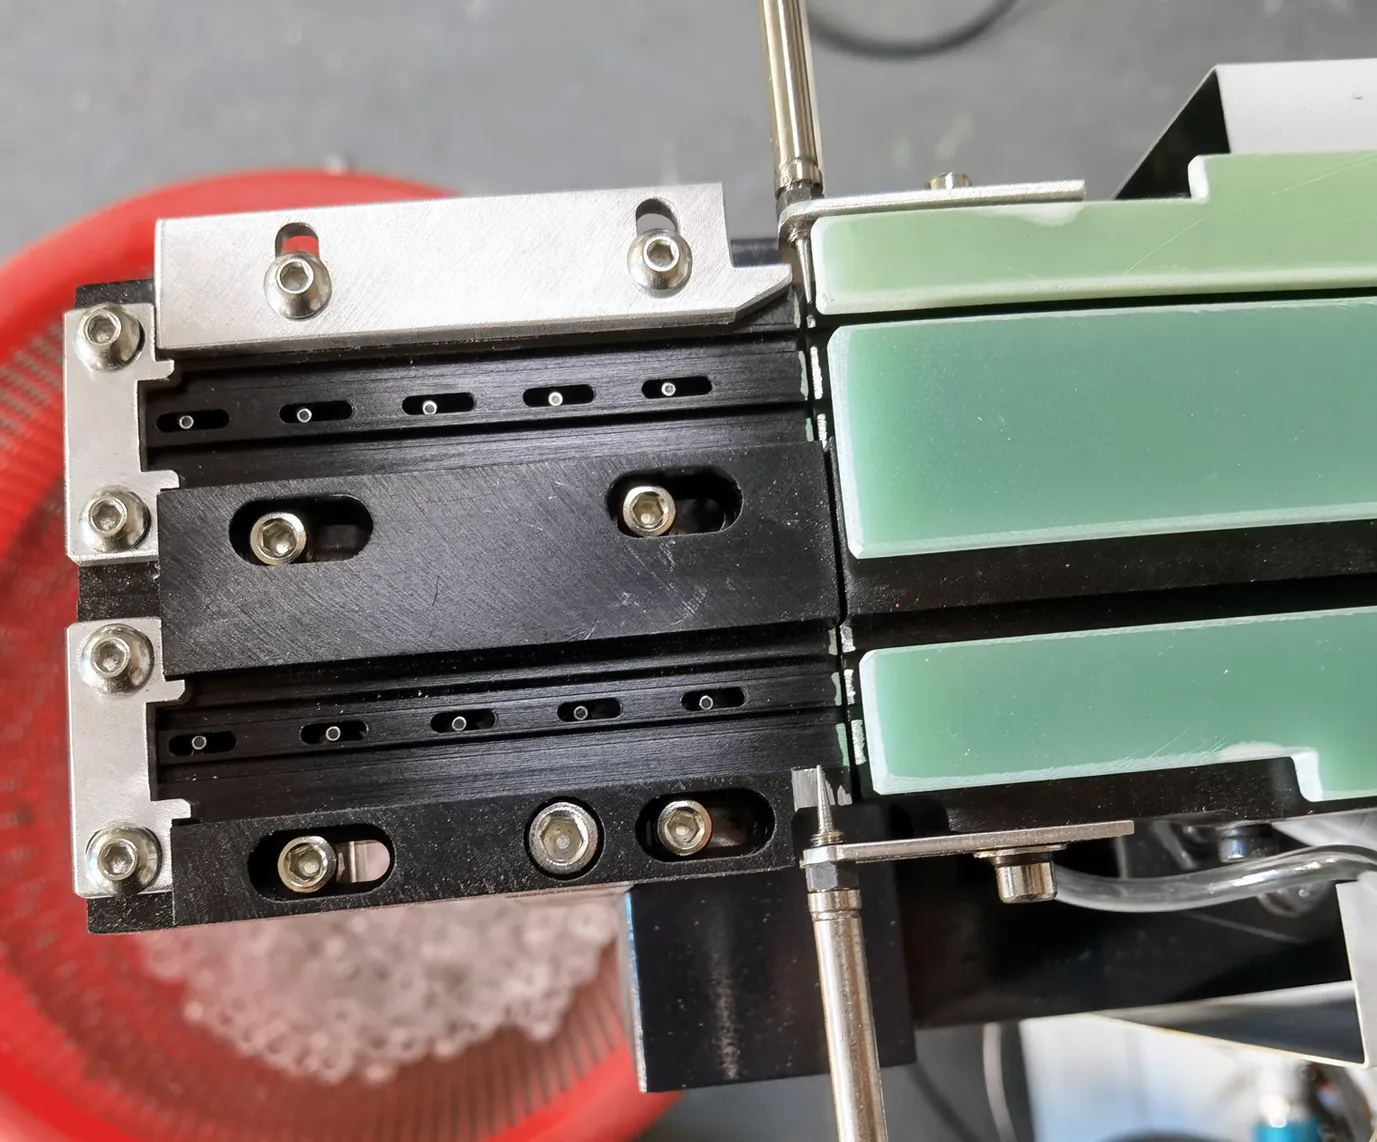
Speed and quality in lens feeding are not separate numbers; they are two views of the same amplitude stability. A channel that holds its amplitude presents every lens at the same speed and orientation, so the nozzle meets a flat, centred lens every cycle within a placement tolerance of ±1 mm.
When amplitude drifts, most cycles still succeed and a small percentage fail — which is exactly what a rejection rate measures. That is why the comparison figures matter: manual lens placement typically runs 5–15% rejection, general-purpose vibratory feeders 2–5%, and the DPS-2 below 0.5% (0.2–0.4% typical after tooling optimisation).
Every figure we quote is measured rather than estimated. Lenses sent for sample testing go through a 48-hour burn-in, and the report contains time-series amplitude and cycle data, a breakdown of rejection causes by category, microscope inspection of lens edges after feeding, and video of the run.
Those measured values are recorded in the machine birth certificate, so the acceptance criteria in the order are the same numbers verified during burn-in. Changeover is the other half of capacity: PLC profile recall takes under three seconds, tool-less adjustment about two minutes, magnetic quick-mount under a minute and verification one to two minutes — under five minutes in total against the 15–30 minutes that manual re-tooling costs.
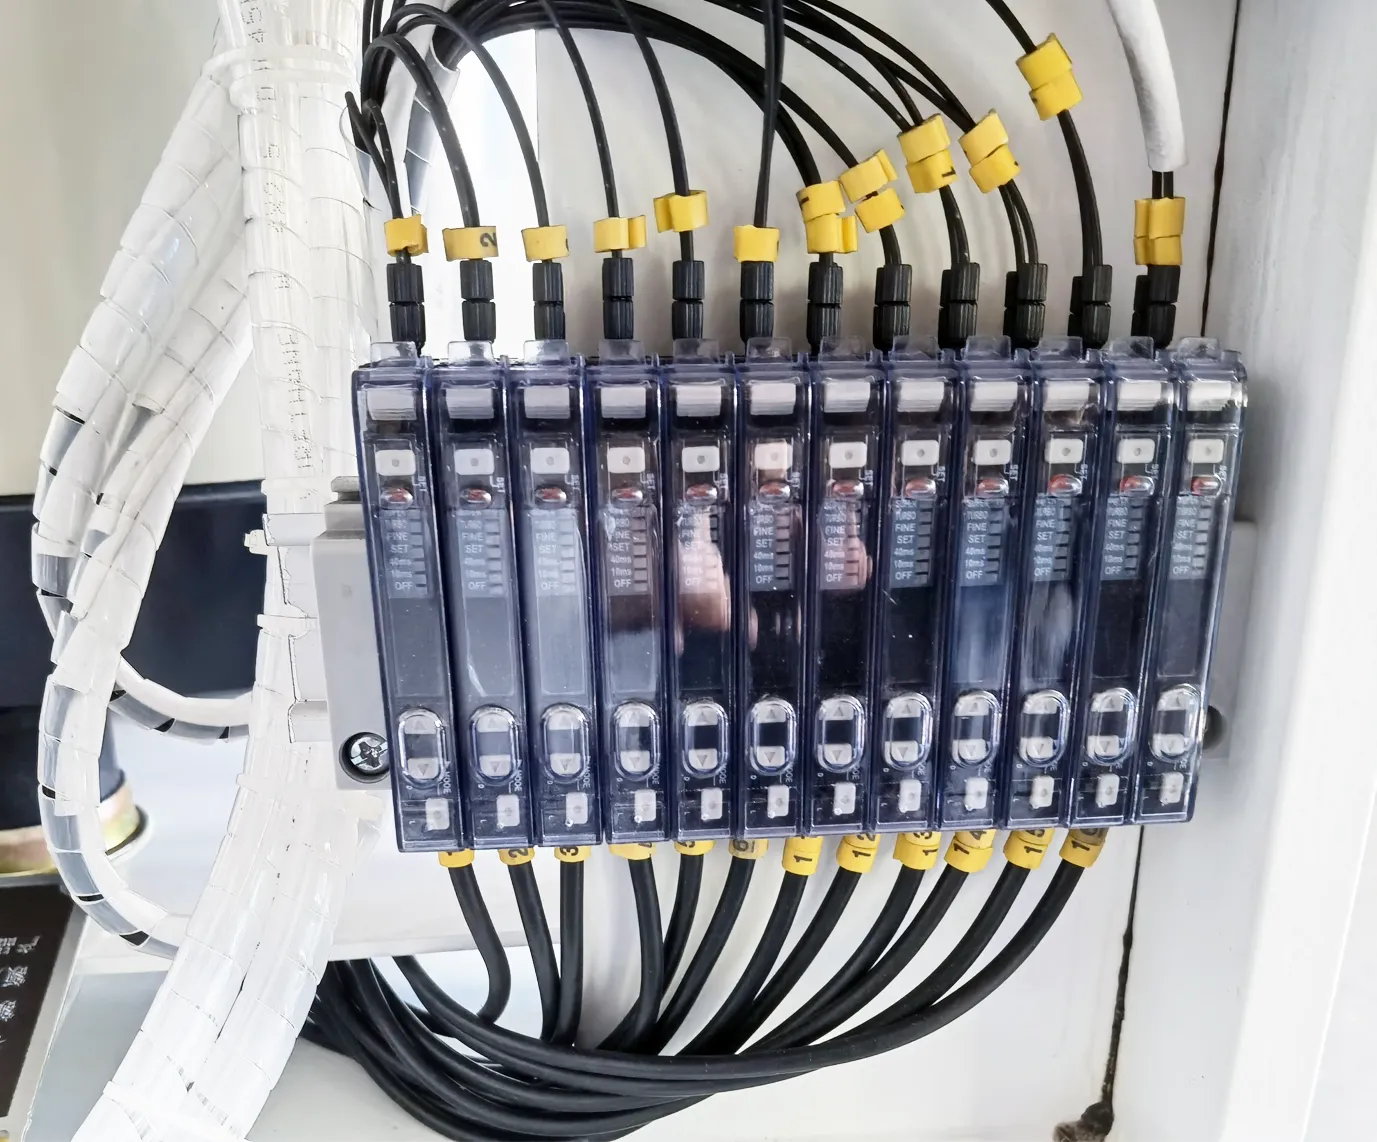
The DPS-2 is quoted against a specific pick-and-place head, not against a machine category. Compatibility is confirmed from three inputs: the machine model and head type, the nozzle or vacuum cup data, and the lens geometry.
In practice most integration work is about presentation height and reach — the pick-up platform is positioned so the nozzle travels the shortest distance from lens to placement — and about the interface between the feeder PLC and the line, which is either discrete I/O or Modbus TCP for lines that want cycle and rejection data in an MES.
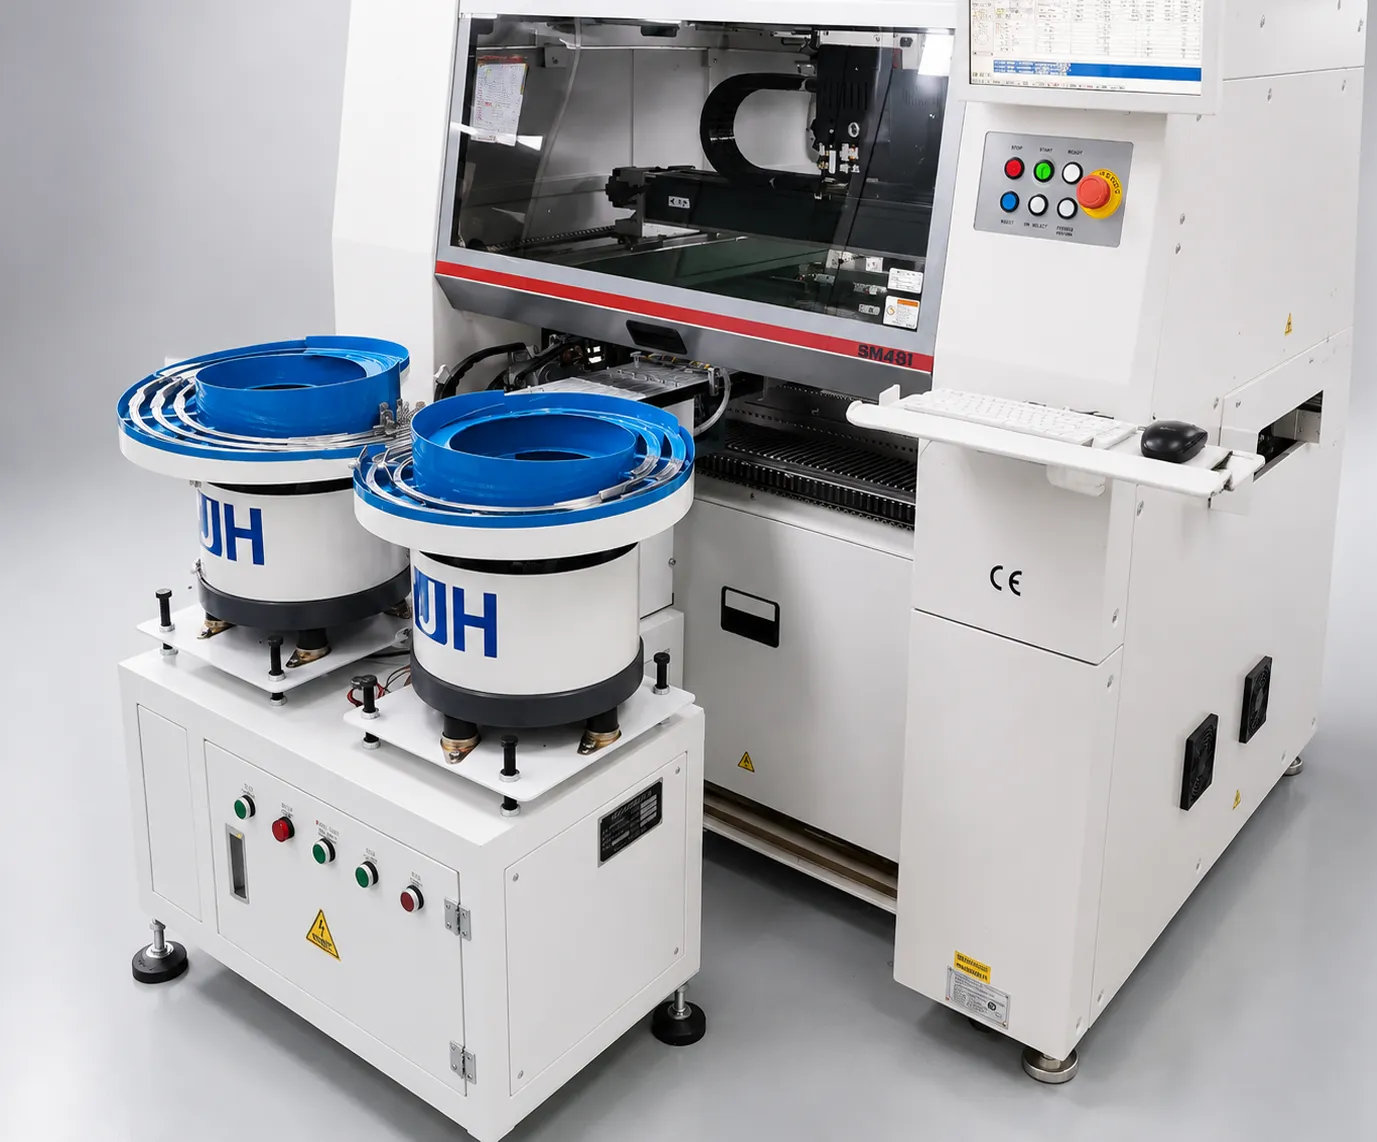
Because the feeder is a stand-alone unit with its own control cabinet, it can be added to an existing line without modifying the pick-and-place machine: the mounting bracket is made for the head, the platform is set to the nozzle, and the recipe is stored in the PLC.
That keeps the installation reversible, which matters when a line is reconfigured later or the feeder is moved to a second machine. Where a customer runs more than one brand on the same floor, one DPS-2 can carry brackets for both, and profiles are recalled by lens rather than by machine.
The table lists the pick-and-place brands the DPS-2 is quoted against and what is documented for each. Model-level confirmation is done from your head and nozzle data during the sample test.
| Pick-and-place brand | Status | What is documented |
|---|---|---|
| Hanwha | Supported | Installations documented on SM481 and SM482 heads |
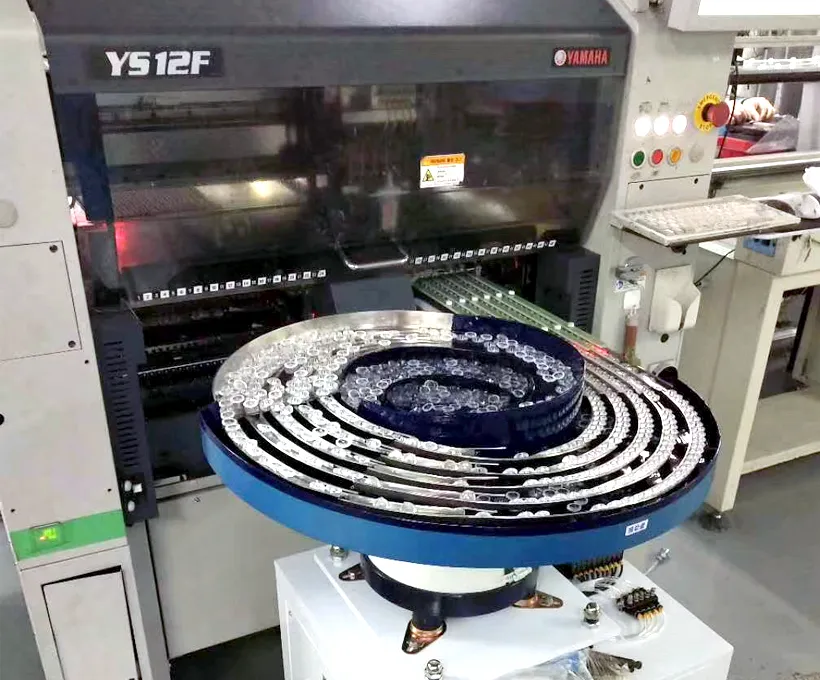
| Yamaha | Supported | Installations documented on YSM10, YSM20R and YSM40R heads |
| JUKI | Supported | Compatibility confirmed from head and nozzle data |
| Samsung | Supported | Compatibility confirmed from head and nozzle data |
| Fuji | Supported | Compatibility confirmed from head and nozzle data |
| Hitachi | Supported | Compatibility confirmed from head and nozzle data |
| Panasonic, Siemens | Assessed per project | Send head drawing and nozzle data for a firm answer |
| Multi-brand line | Supported | Brackets for both heads, profiles recalled by lens type |

Tooling covers lenses from 3 mm to 25 mm in diameter. Within that band the DPS-2 handles round lenses, three-foot, four-angle and rectangular cutout geometry as standard; asymmetric or unusual outlines are treated as a custom track tooling project, priced per lens type rather than per machine.
The tooling for a given lens is what sets orientation quality, so it is developed and verified on your actual parts: lenses are sent in batches of 500–800 per type, the 48-hour burn-in runs with those parts, and the tooling is adjusted until orientation and rejection are repeatable across a full shift rather than only at the start.
Three practical limits are worth knowing before you specify. First, lens size is not the only factor — surface finish matters, because coated or sensitive optical surfaces are fed with gentler bulk movement and a longer alignment path rather than higher amplitude.
Second, very small lenses reduce the usable escapement width, which lowers the practical feed rate per channel; the tooling still works, but the cycle follows the lens. Third, cleanroom and ESD requirements are configuration choices made at order time, not retrofits: conductive bowl coating, static-dissipative inserts and a HEPA-filtered cabinet are specified together so the machine passes an ESD audit and IQ/OQ/PQ validation in one pass.
The commercial model is deliberately simple, and the answers to Q13–Q20 above are the authoritative version; this section collects them for planning. A base DPS-2 starts around $8,000 USD, with the typical configured machine between $8K and $12K depending on channel count and options, and a spare parts kit at $500–800.
Minimum order quantity is one unit, with volume discounts at 5, 10 and 20 units — the first machine and the fiftieth receive the same engineering attention, including sample testing, the 48-hour burn-in, 120-point QC and operator training. Payment is 70% T/T deposit with the order and 30% T/T before shipment, with L/C at sight available to existing customers.
Lead time is 15–20 working days for a standard machine or 10 days for an express build, followed by 5–7 days by air or 15–35 days by sea, giving 24–62 days door to door; DDP is available and removes clearance from your side of the project, with progress updates through the build.
Warranty is one year comprehensive covering parts and labor, remote diagnostics within 12 working hours (Mon–Sat, 09:00–23:00 China Standard Time, UTC+8) and parts dispatched within 48 hours by DHL, with free technical support for the life of the machine and extended cover of two or three years available. Sample testing is free, and lenses are returned with the machine.
Specification summary for the standard DPS-2 configuration, as published in the answers above.
| Parameter | Specification |
|---|---|
| Function | Automatic lens presentation to pick-and-place nozzle |
| Channels | 3–6 standard, up to 10 custom, independent drives |
| Feed rate | 0.5–1 sec/lens/channel — 3,600–7,200 UPH/channel |
| Rejection | Below 0.5%, typically 0.2–0.4% after optimisation |
| Lens range | 3–25 mm, round / three-foot / four-angle / rectangular cutout |
| Placement tolerance | ±1 mm |
| Control | Mitsubishi FX5U-32MT/ES + 7-inch Weintek HMI, 50 profiles |
| Sensing and communication | Keyence sensors, Modbus TCP to MES |
| Power and air | 220 V AC single-phase 0.55 kVA, 0.4–0.6 MPa air |
| Footprint and weight | 1050 × 700 × 750 mm, ~130 kg, <65 dB(A) |
| ESD and cleanroom | 10⁶–10⁹ Ω bowl coating, ISO Class 7 configuration option |
| Changeover | Under 5 minutes for a lens change |
The forty questions below are grouped by the order in which they usually arise in a project. Questions 1–12 are technical and answer whether the machine fits your lens, your machine and your line; 13–20 are commercial and answer cost, lead time, warranty and shipping; 21–28 cover service after installation; 29–35 cover environment, ESD and cleanroom; 36–40 deal with trade, Incoterms and payment protection.
Two habits make the answers more useful. First, treat any figure that depends on your lens as provisional until a sample test has been run: feed rate and rejection are measured properties, not catalogue claims. Second, when you request a quotation, include the eight details in the checklist above plus your machine model and nozzle data, which is enough to answer compatibility and price in one round and to schedule the sample test in the same reply.
Topic index: which group of questions to read for each stage of a project.
| Questions | Topic | Read this when |
|---|---|---|
| Q1–Q6 | Product and capacity | You are checking whether the machine meets the requirement |
| Q7–Q12 | Control, maintenance, Industry 4.0 | You are specifying the line interface |
| Q13–Q20 | Cost, ROI, lead time, warranty, shipping | You are preparing a budget or a purchase file |
| Q21–Q28 | Support, spares, installation, certifications | You are planning service after installation |
| Q29–Q35 | Industries, cleanroom, ESD, life, sustainability | Your line is audited or regulated |
| Q36–Q40 | Customs, Incoterms, payment, logistics | You are placing the first order |
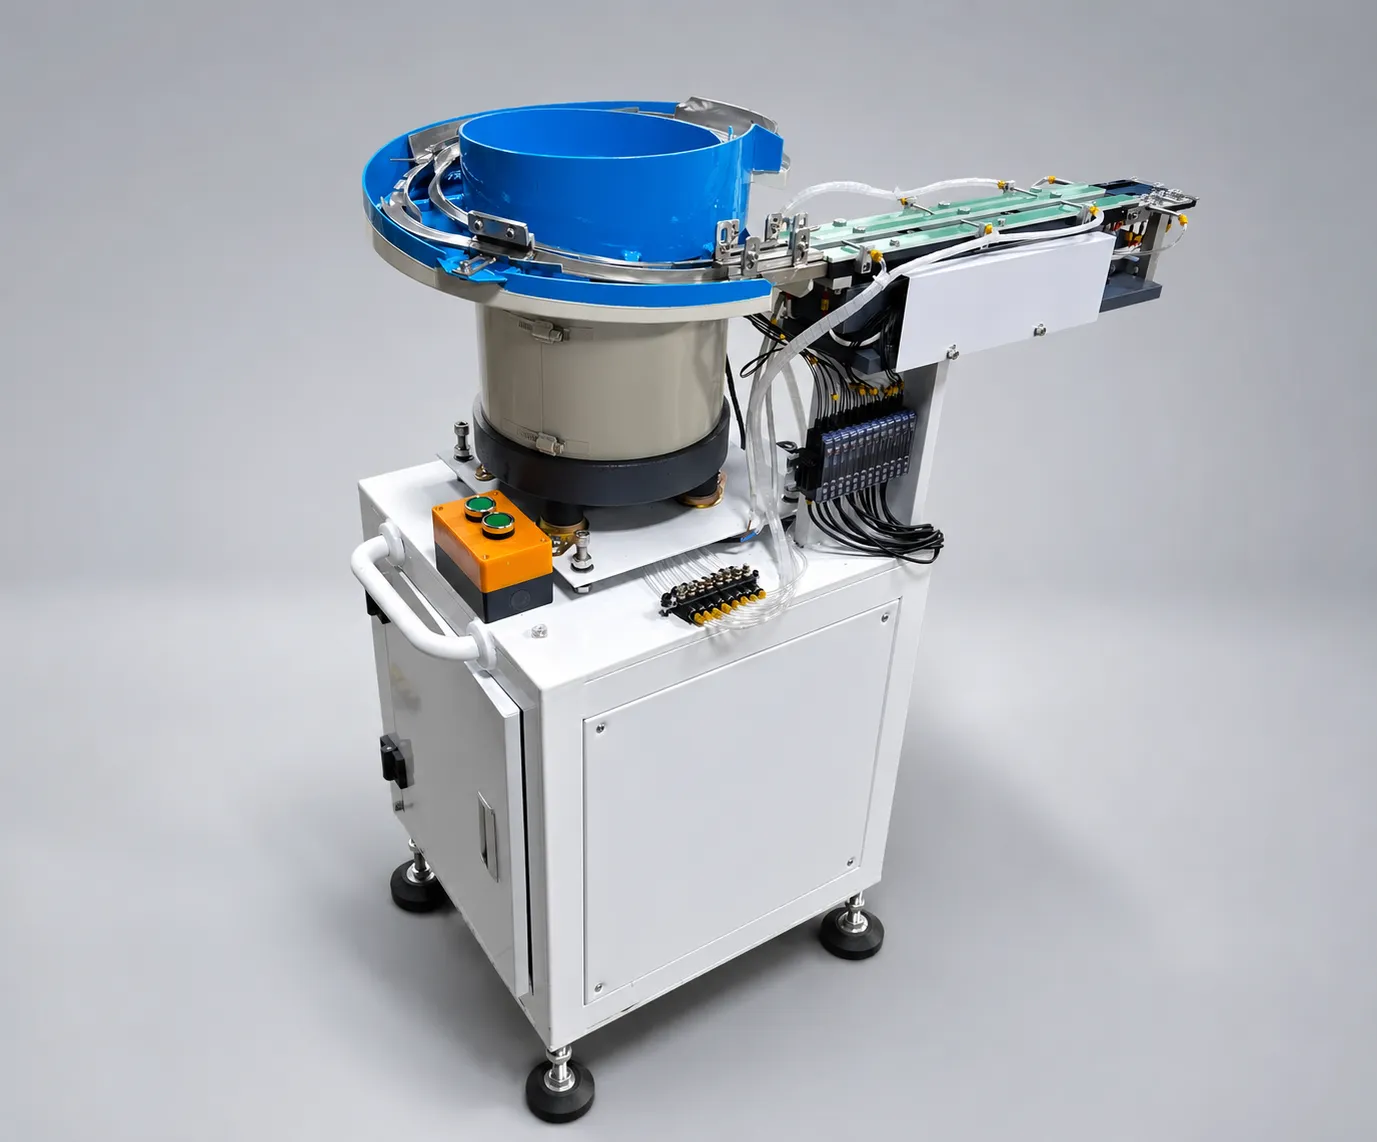 RecommendedJHIMS DPS-2Lens vibratory feeder for SMT pick-and-place · 0.5–1s per lens · <0.5% rejection · ±1mm alignment.View product →
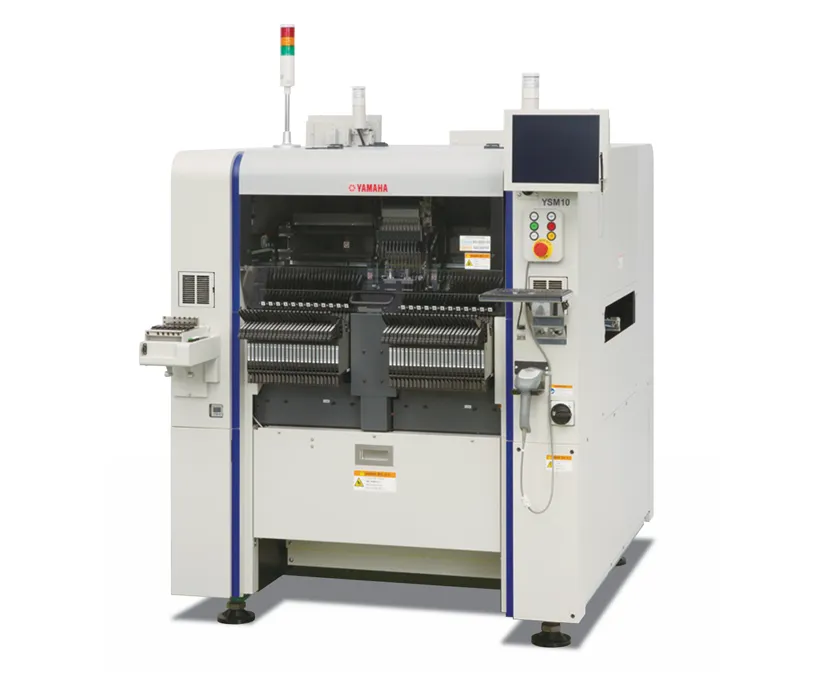 CompanionYamaha YSM10 MounterHigh-speed compact modular mounter – 46,000 CPH, 96 feeders, e-Vision + Side View.View product →
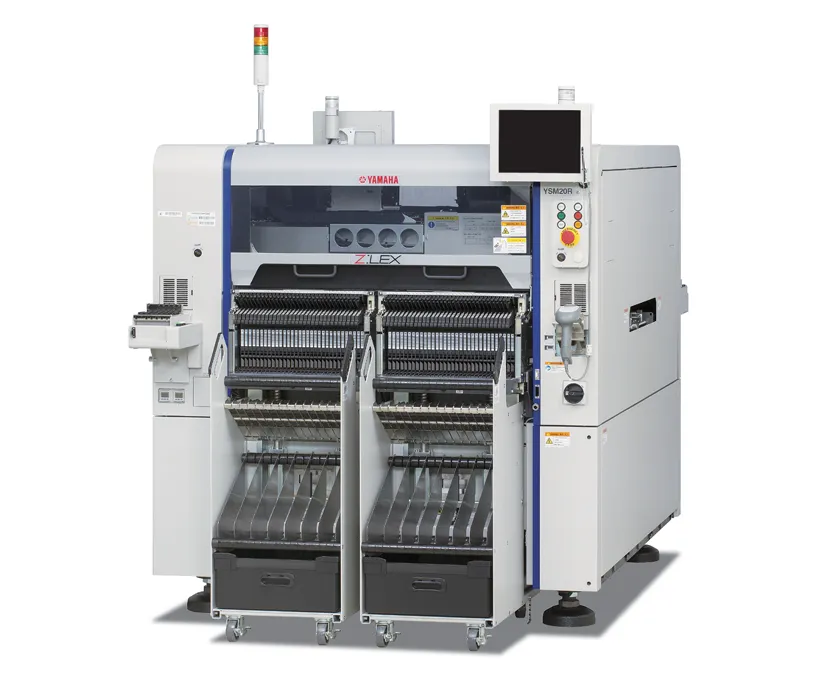 Yamaha YSM20R Pick and Place95,000 CPH modular mounter — pairs with DPS-2 lens feeding lines.View product →
 3D SPI Solder Paste InspectionCatch printing defects before reflow with 100% 3D paste inspection.View product →
 R10 Reflow OvenLead-free hot air reflow with stable thermal profiling for lens assemblies.View product →
 D900 Dispensing MachinePrecision dispensing for conformal coating and lens bonding steps.View product →
 Buying GuideHow to Choose an SMT Lens Feeder (2026)An 8-step buying path, supplier scorecard and dual vs single frequency comparisonRead article →
 Case StudySMT Lens Feeder ROI Case StudyReal KPI transition: defect rate 12%→0.3%, UPH 900→3420, 7-month paybackRead article →
 GlossarySMT Lens Feeding GlossaryTerminology for vibratory feeding, PID control, and UPH metrics.Read glossary →
 ComparisonDual vs Single Frequency Vibratory FeederTechnical comparison of the two vibration technologiesRead article →
 ComparisonManual vs Automatic SMT Lens FeederWhich feeding method is right for your production?Read article →
 ProductDPS-2 Product KnowledgeWhat the DPS-2 is, how it works, and what it can feed.Read more →
Ask our engineers anything about the DPS-2 — compatibility, lens testing, delivery, or pricing — and get an answer — first reply within 12 working hours (Mon–Sat, 09:00–23:00 China Standard Time, UTC+8).
Prefer to see it before you ask? Watch the DPS-2 automatic lens vibratory bowl feeder and the lens feeder running on a pick-and-place line, or send your lens photos on WhatsApp for a direct answer from an engineer. More machine videos: JHIMS on YouTube.
Real deployment: how a lens-module maker in Xiamen ended repeat feeder purchases — DPS-2 lens feeder repeat-purchase case study.


