Address
Building A1, Runteng Industrial Park, No. 4 Xishan Road, Longteng Community, Shiyan Subdistrict, Bao'an District, Shenzhen 518000, China
Work Hours
Monday to Saturday: 09:00 – 23:00 (UTC+8)
Sunday: closed
Address
Building A1, Runteng Industrial Park, No. 4 Xishan Road, Longteng Community, Shiyan Subdistrict, Bao'an District, Shenzhen 518000, China
Work Hours
Monday to Saturday: 09:00 – 23:00 (UTC+8)
Sunday: closed

Video tutorial for the JHIMS L5 solder paste printer — the seven operating steps, the fault diagnosis table, maintenance cycles, parameters, and the operator mistakes that cause most print defects.
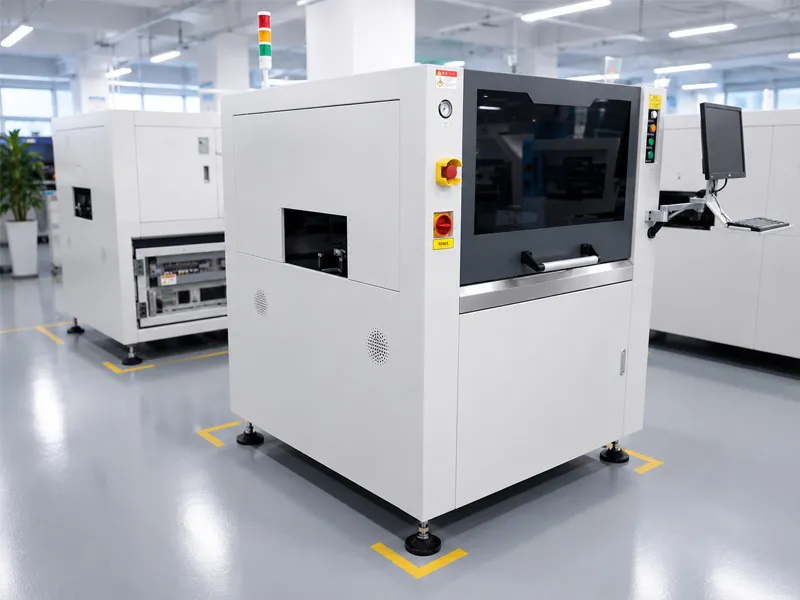
Video tutorial for the JHIMS L5 solder paste printer — the seven operating steps, the fault diagnosis table, maintenance cycles, parameters, and the operator mistakes that cause most print defects.

Click any step to open that tutorial video. The main player above shows the full 7-step sequence — click a step to play it in place.
Before moving the machine, lock the L5 to prevent damage during transport. After the machine arrives at its new location, remove the locking block before powering up. Back up the system data to prevent loss — the backup protects your programs, parameters and calibration data during relocation or maintenance.
Connect the signal cables (24V/0V) and set up the 220V power supply. Maintain the required air pressure between 0.5–0.6 MPa (see the official specification: 4–6 kgf/cm² air supply). Verify all connections before switching on, then start the software and confirm the machine initializes without alarms.
Run the pre-startup checks, then navigate the software interface. The system detects errors and displays them clearly; switch the interface language as needed. Understand the permission levels (operator, technician, engineer) — each role has different access rights. Investigate any abnormal noise or malfunction before continuing production.
Create a new program and input the PCB size parameters. Select the recognition mode (PCB marks or stencil marks) and adjust the cleaning settings (wet, dry or vacuum). Proper setup ensures precise alignment between the stencil and the PCB for optimal printing results. For extra-large panels, JHIMS also builds the L12 fully automatic visual solder paste printer, which prints up to 1,200 × 350 mm with the same 2D paste-inspection workflow.
Fine-tune the PCB setup, recognition modes and cleaning adjustments from Step 4. Advanced programming ensures accurate solder paste application for complex PCB designs, including fine-pitch boards (down to 0201 components and 0.25mm pitch supported).
Configure the alcohol spray settings — spray offset, length and speed — together with the PCB/stencil separation distance and squeegee parameters. Set the separation in three stages for clean release, and adjust the printing speed (10–200mm/s) and pressure (0.5–20kg) for the paste type and aperture size.
Install the scraper (rubber or steel squeegee, 45°/55°/60° angle) and set up the template cleaning paper. Secure the cleaning paper and manage the alcohol level for effective stencil cleaning. The L5 supports dry wipe, wet wipe and vacuum cleaning modes to keep apertures clear between batches.
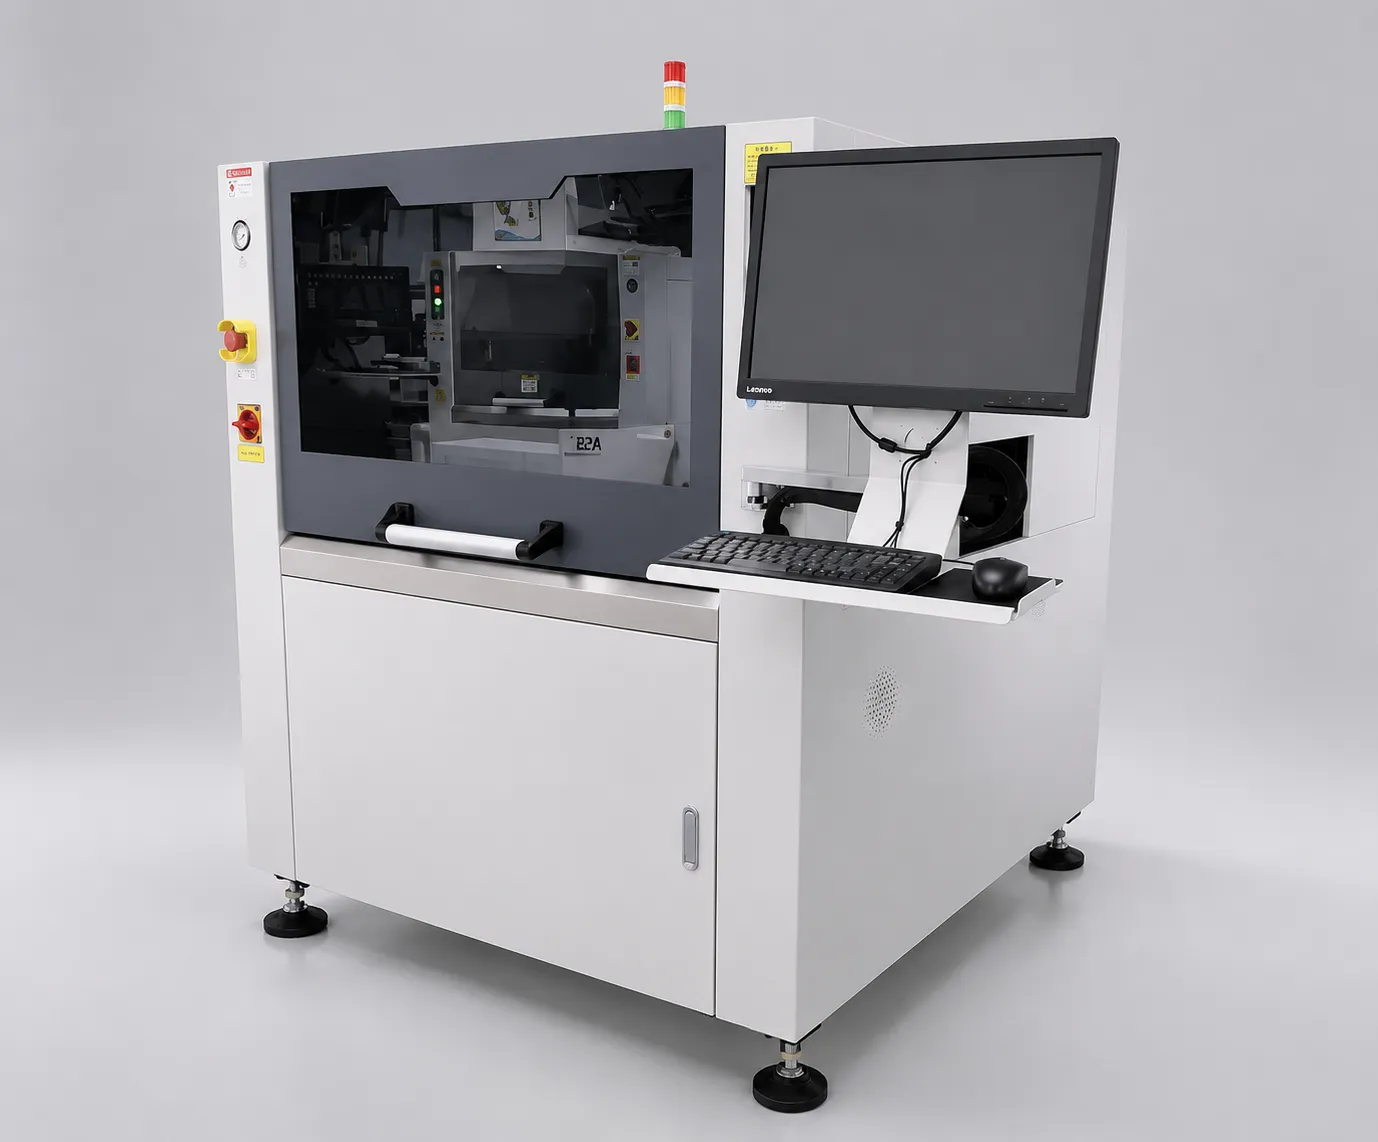
Stencil printing is as much a rheology problem as a mechanics one. Solder paste is thixotropic: under the shear of the squeegee it thins and flows into the stencil apertures, then thickens again the instant it stops, holding its shape on the pad. The variables that decide whether that deposit is flat, crisp and repeatable are paste viscosity (as delivered and as it ages), stencil thickness and aperture design, and squeegee pressure, angle and speed. When these drift you get the classic defects — slumping and bridging, open joints, or a deposit that looks right on the board but does not reflow correctly. The sections below are the working knowledge that goes beyond the operator manual: how to diagnose a fault, the consumables and filters that keep the machine healthy, the maintenance cycle that stops drift before it starts, and a fast parameter reference for a correct setup on the floor.
| Symptom | Probable Cause | Probability | Correction |
|---|---|---|---|
| Incomplete prints / skip-print | Stencil apertures blocked with dried paste | 35% | Run cleaning cycle; if blocked, manual solvent clean |
| Incomplete prints / skip-print | Squeegee pressure too low | 15% | Increase pressure in small steps; verify air supply |
| Smearing / bridging | Squeegee pressure too high or edge worn | 20% | Reduce pressure; inspect/replace scraper edge |
| Registration drift | Fiducial teaching error or stencil loose | 15% | Re-teach fiducials; check stencil tension |
| Thin prints | Separation speed too fast | 10% | Slow stencil-PCB separation speed |
| False 2D alarms | Inspection thresholds too tight | 5% | Loosen thresholds; re-teach inspection windows |
| No print on part of the board | Stencil warped or not seated flat; board support pins missing | – | Check stencil flatness and clamp; add support pins under warped areas |
| Excess solder paste | Squeegee pressure too high or speed too low | – | Reduce pressure; increase speed |
| Excess solder paste | Stencil-PCB separation too fast | – | Slow the separation speed |
| Insufficient paste | Squeegee blade worn or damaged edge | – | Replace the squeegee blade |
| Insufficient paste | Stencil apertures undersized or clogged | – | Verify aperture-to-pad ratio; run cleaning cycle |
| Bridging | Paste viscosity too low | – | Check paste viscosity; re-condition the paste |
| Bridging | Squeegee angle incorrect | – | Verify the squeegee angle (45°/55°/60° default) |
| Print shift | PCB not clamped or support pins not set | – | Verify PCB clamping and support pin layout |
| Print shift | Stencil off-center | – | Re-align the stencil to the PCB |
| Registration drift | Stencil tension lost | – | Check stencil tension and re-tension if needed |
| Registration drift | CCD lens dirty – mark recognition unstable | – | Clean the CCD lens; re-teach fiducials |
| 2D misses defects | Inspection thresholds too loose | – | Tighten thresholds; re-teach windows |
| 2D false alarms | Camera misaligned or window drift | – | Re-calibrate the 2D camera position and windows |
| Solder paste spilling | Squeegee pressure too high | – | Reduce pressure; check blade edge |
| Skipped prints | Stencil cleaning not triggered between batches | – | Verify cleaning cycle frequency in the program |
| Air pressure low alarm | Air supply insufficient; regulator not set | – | Check the air compressor and regulator; set 4-6 kgf/cm² |
| Maintenance Area | Check & Maintenance Content | Tools |
|---|---|---|
| 1. Platform | Check mounting screws for looseness; clean oil and paste residue; keep work surfaces clean; lubricate ball screws and linear guides. | Grease gun, lint-free cloth |
| 2. Squeegee | Check screws, plugs and connectors for looseness; remove foreign objects; check squeegee traverse belt wear and screw tightness; lubricate ball screw if fitted. | Grease gun |
| 3. Cleaning unit | Check the cleaning unit for deformation; roller motor paper feed; wiper bar wear; spray valve jetting; cleaning tube corrosion/leaks; spray belt wear. | — |
| 4. Vision CCD | Check camera mounting screws and connectors; remove falling debris; confirm image clarity; check stop-cylinder air leaks. | Lint-free cloth |
| 5. Stencil frame | Check the stencil frame for deformation, cleanliness and wear; cylinder air leaks; air tube wear; left-right frame parallelism. | — |
| 6. Conveyor | Check rail screws; oil/paste residue; transport belt wear or breaks; rail height consistency (no flaring); stopper screw wear. | — |
| 7. Electrical | Measure ground continuity with a multimeter; air pressure gauge; drain filter water; cylinder air leaks; terminal wiring; motion control card; chassis and IPC fans; origin/limit switches. | Multimeter |
| 8. Enclosure | Wipe the enclosure with a lint-free cloth and a little WD-40 cleaning oil. Never use water or an air gun. | Lint-free cloth, WD-40 |
| 9. Level | Place a spirit level on the platform and verify the machine is level. | Spirit level |
| Parameter | Recommended | Allowed Range | Notes |
|---|---|---|---|
| Screen frame size | 370×370 – 737×737 mm | Frame thickness 20–40mm | Standard frames |
| PCB size | 50×50 – 400×340 mm | 510×340mm option | Warpage <1% |
| PCB thickness | 0.4 – 6 mm | Board edge clearance 2.5mm | Board height 25mm |
| Printing speed | 10 – 200 mm/s | Adjustable | Slower for fine pitch |
| Printing pressure | 0.5 – 20 kg | Adjustable | Rubber or steel squeegee |
| Printing accuracy | ±0.025 mm | — | With vision alignment |
| Repeat position accuracy | ±0.01 mm | Machine spec | CCD mark-point alignment |
| Cycle time (excl. cleaning) | 7 s | 14 s incl. cleaning | Changeover 5 min |
| Squeegee | Rubber / steel, 45°/55°/60° | Single or double | Per paste & aperture |
| Cleaning modes | Dry / wet / vacuum | Spray cleaning system | Auto stroke generation |
| Camera | 1.3 megapixel digital | FOV 10×8mm | Geometric matching vision |
| Mark points | 0.1 – 6 mm, max 4 | Standard shapes | 2D: low tin / bridging |
| Air required | 4 – 6 kgf/cm² | ~5 L/min | Check before each shift |
| Power input | AC 220V ±10%, 50/60Hz, 2.5kW | — | PC control |
| Machine weight | ~1000 kg | 1220×1375×1500mm | — |
The 2D inspection camera scans the deposited paste pattern after printing. By measuring the area of each paste deposit against the stencil aperture area, the system detects insufficient paste (area too small), excess paste (area too large) and bridging (paste connecting adjacent pads). It cannot measure height directly — that requires 3D/SPI — but area-based detection catches most print defects before reflow.
Defects caught at the printer cost seconds to fix (clean stencil, reprint). Defects caught after reflow cost minutes or hours (desoldering, rework, or scrapping). The 2D inspection is the cheapest quality gate in the entire SMT line.
A poorly taught fiducial shifts every print on the board. The error compounds across the board — a 0.1mm mark error at the origin becomes a 0.5mm shift at the far corner for a 300mm board. Teach marks carefully with the crosshair zoomed in.
The L5 supports 0201 components and 0.25mm pitch. For such fine-pitch boards, use diagonal marks, lower pressure, slower speed and three-stage separation to keep registration and release consistent.

These six mistakes share one characteristic: each of them looks like a shortcut and costs more time than it saves. Removing the transport lock block is the clearest example — it takes seconds and skipping it risks damaging the print head and drives, which is a service event rather than a delay. The pre-startup air pressure check matters for a similar reason: printing and stencil cleaning both run on air, so a supply below the 4–6 kgf/cm² band produces false alarms and unstable deposits that operators then try to correct with parameter changes, moving a clean machine away from a known-good recipe. Teaching a single fiducial cannot correct board rotation, so registration errors appear as intermittent misalignment that is very hard to diagnose later; two marks solve it at the start.
The remaining three are process discipline. Fine-pitch boards need lower squeegee pressure and slower speed than the defaults, because default settings smear fine apertures even though they work on coarse boards. Repeated 2D inspection alarms should be read as a real process drift rather than an alarm to silence; disabling the check removes the cheapest quality gate on the line. And mixed or expired solder paste contaminates apertures and produces skip-print defects that look like a printer fault but are a material fault, so paste identity and expiry are part of the printing process rather than a stores issue.
What makes these seven rules worth following is that each one is a habit rather than a task. Backing up system data before relocating a machine or changing hardware costs minutes and decides whether a recovery is a restore or a re-teach. Checking air pressure before every shift takes seconds and removes the most common cause of unstable printing. Matching squeegee type — rubber or steel, in 45°, 55° or 60° profiles — to the paste and aperture geometry is a decision that should be made once per product and then recorded, not re-invented per shift. Three-stage separation for fine-pitch boards is the difference between clean release and paste strings that bridge the next print.
The last three rules are about visibility. Cleaning the CCD lens weekly keeps vision quality predictable, and vision drives both alignment and 2D inspection, so a dirty lens degrades two functions at once. Verifying the first board every shift takes about 30 seconds and catches drift before a batch is produced rather than after it is inspected. Documenting threshold settings with each recipe means that when quality does drift, the operator can compare against a recorded baseline instead of guessing what changed — which is the single most useful piece of documentation a printing process can have.
RelatedJHIMS L5 Solder Paste PrinterFully automatic visual solder paste printer with ±0.025mm accuracy and integrated 2D inspection.View product → RelatedJHIMS M8 Solder Paste PrinterFully automatic vision solder paste printer for larger boards — CCD alignment (±0.01mm) and 2D inspection.View product →
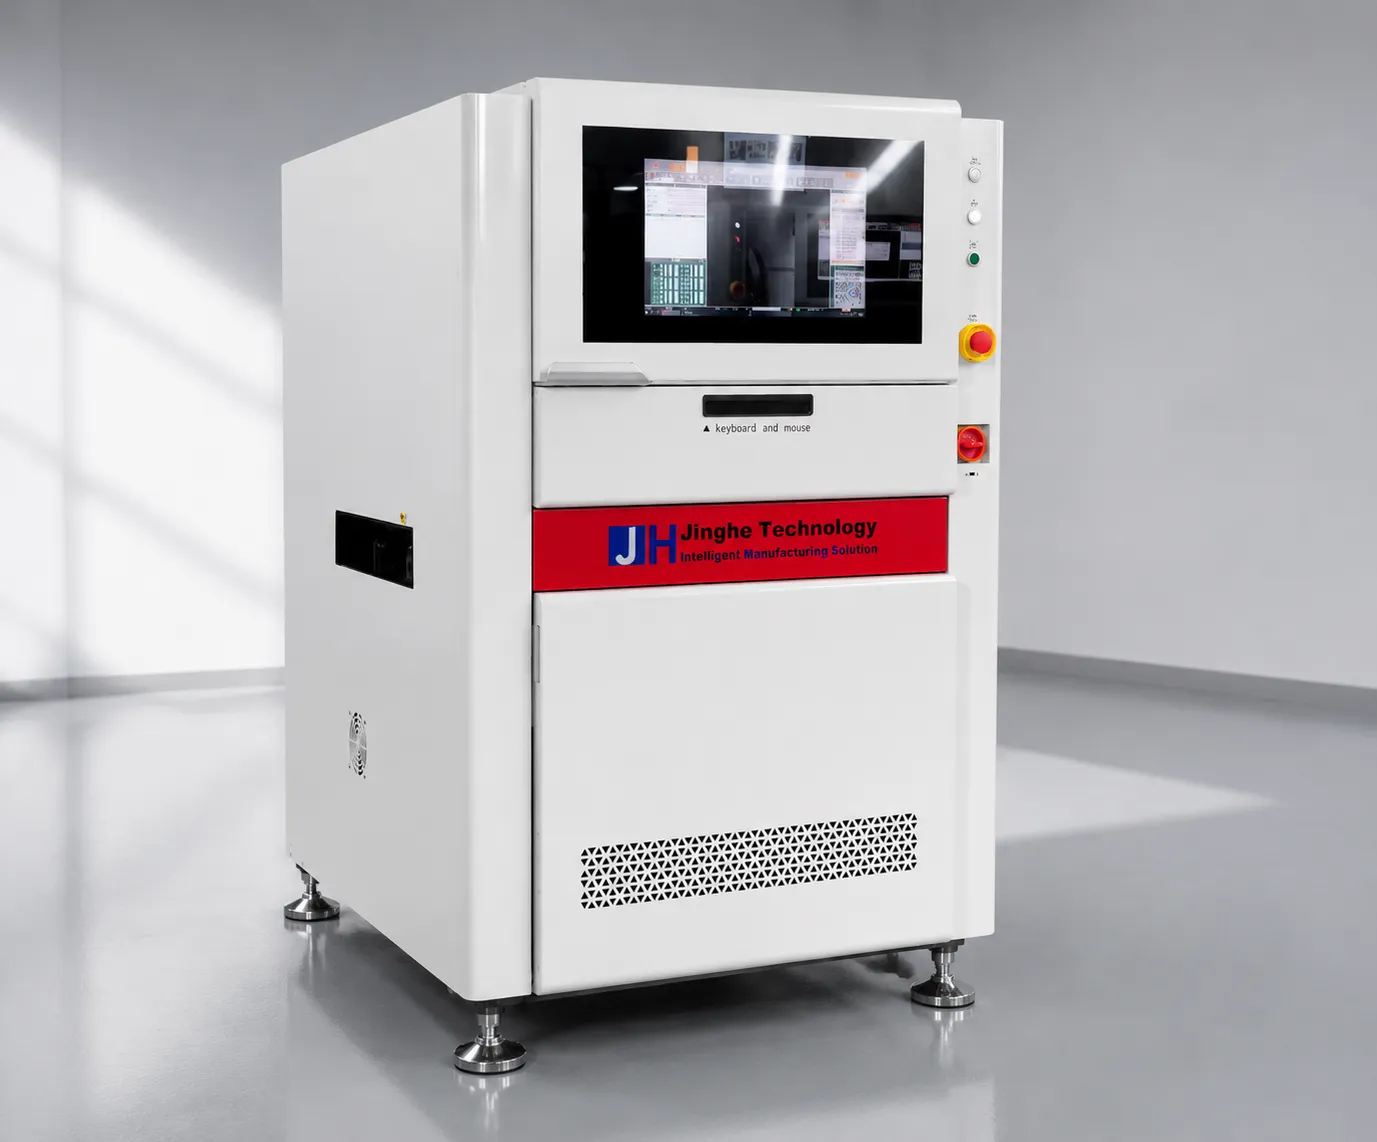 RelatedJHIMS R6-U UV Laser Marking Machine355nm UV laser marker for PCB traceability — QR and Data Matrix codes at high throughput.View product →
 RelatedJH-D900 Glue Dispensing MachineHigh-precision automatic glue dispensing for SMT assembly — solder paste, adhesive and coating.View product →RelatedJHIMS S630 3D SPI3D solder paste inspection for SMT lines — detects volume, height and area defects before reflow.View product →
 RelatedJHIMS R10 Reflow OvenLead-free hot-air reflow soldering for SMT lines — 20 heating zones, up to 300°C peak.View product →
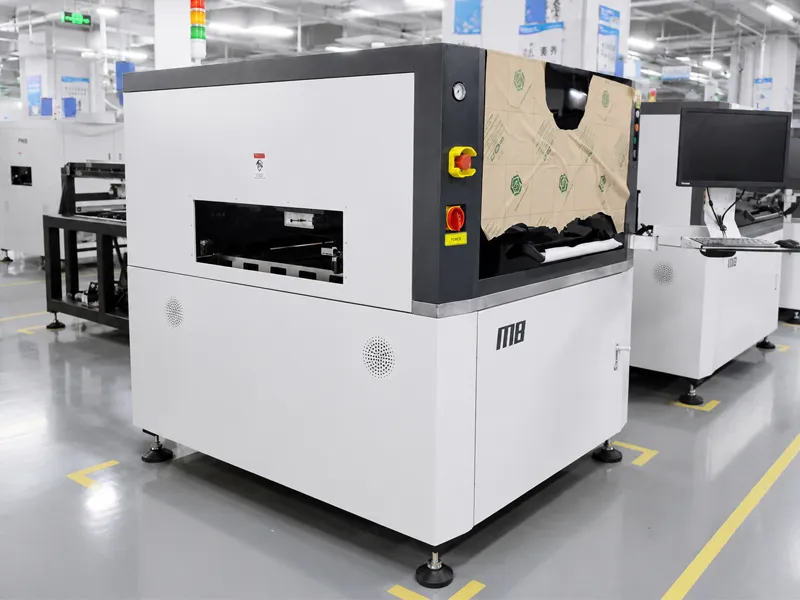 GuideM8 Solder Paste Printer GuideStep-by-step video guide for operating the JHIMS M8 solder paste printer.Read article →
 GuideR6-U UV Laser Marking Machine Guide9-step video guide: installation, laser calibration, QR marking workflow and troubleshooting.Read article →GuideD900 Dispensing Machine GuideStep-by-step video guide for operating the JH-D900 glue dispensing machine.Read article →Case StudyM8 Solder Printer Case StudyHow a Saudi Arabia LED plant uses the JHIMS M8 for mini-LED board printing.Read article →
 GuideDPS-2 Lens Feeder Troubleshooting Guide5 common lens-feeder issues ranked by probability with step-by-step fixes — most resolved in under 10 minutes.Read article →SupportTechnical SupportTraining, remote diagnostics and spare parts dispatch for your JHIMS line.Read article →
Contact our engineers for a free evaluation, first reply within 12 working hours (Mon–Sat, 09:00–23:00 China Standard Time, UTC+8).



