Address
Building A1, Runteng Industrial Park, No. 4 Xishan Road, Longteng Community, Shiyan Subdistrict, Bao'an District, Shenzhen 518000, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
Building A1, Runteng Industrial Park, No. 4 Xishan Road, Longteng Community, Shiyan Subdistrict, Bao'an District, Shenzhen 518000, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM

An LED cabinet maker in Argentina replaced manual screw tightening with a JHIMS BL18: repeatable torque, faster cabinets.

How an LED display cabinet manufacturer in Argentina moved from manual screw tightening — cycles that depended on the operator and torque that varied from screw to screw — to a JHIMS BL18 vertical four-axis screw fastening machine.
At a glance: who the customer is, where the machine was delivered, and what drove the investment.
LED display manufacturing in Argentina is a competitive, export-facing segment, and cabinet quality is judged by customers who see the finished wall rather than the assembly bench behind it. A cabinet that does not close cleanly or a joint that loosens in service is visible on site.
That is why the project was framed around consistency as much as speed. Faster cabinets from a bench that tightens to a different torque on every screw only moves the problem downstream, so the requirement from the start was a machine that applies the same fastening on every cabinet.
LED display cabinets are assembled from sheet-metal and aluminium profiles, and every module or board is held in place by M4 fasteners. Before this project the customer’s operators tightened those screws by hand with electric or manual drivers at the assembly bench — the same fastening method used across the cabinet shop for years.
Manual tightening has two costs that only show up at volume. The first is pace: every screw has to be picked up, positioned, driven and checked by a person, so finished cabinets track how fast an operator can work.
The second is consistency: hand tightening delivers whatever torque the operator applies, so clamping force varies between screws and between operators.
Those two costs are what pushed the project. Cabinet orders were growing, and the difference between a cabinet that closes cleanly and one that needs rework was being decided by an operator’s technique rather than by a setting on the machine.

Every reported problem traces back to one property of manual tightening: the fastener receives torque from a human hand, and a hand is not a calibrated tool. Two operators with the same driver will not deliver the same clamping force, and the same operator will not deliver it at 08:00 and at 17:00.
Cycle time follows from the same cause. In manual assembly the screw is the smallest unit of work and the operator carries all of it: fetch, place, drive, verify. Automation does not make the screw faster in isolation — it removes the operator from that sequence and lets cabinet assembly continue in parallel.
The reported challenges, their cause when screws are tightened by hand, and the design response.
| Reported challenge | Why it happens with manual tightening | Design response |
|---|---|---|
| Torque varies between screws | A hand driver applies whatever force the operator gives it | Fastening is applied by the machine at a programmed setting |
| Output depends on operator pace | One person performs fetch, place, drive and verify per screw | The head travels and drives under program control |
| Fatigue during the shift | Repetitive tightening degrades technique over hours | The machine repeats the same cycle from the first cabinet to the last |
| No reusable pattern per cabinet | Screw positions are found by eye for every new batch | 1,000 stored programs, camera-assisted alignment for positioning |
| Loading stops fastening | The bench works on one cabinet at a time | Dual fixtures: the next cabinet is assembled while the other is fastened |
Before ordering the BL18, the project set six requirements the machine had to meet:
The six requirements describe one change: move the decision about torque and position off the operator and onto the machine, without making the machine harder to run than the bench it replaces.
The fixture size is the practical constraint. Cabinets are large, so the machine has to accept the full cabinet rather than a module, and the clamping has to hold it flat enough for the screw to seat without the panel flexing away from the head.
Why JHIMS: the machine is built around the customer’s own cabinet fixture rather than a standard work envelope, and the fastening pattern is taught from the cabinets that will actually run on it.
The configuration answers the two problems in the order they were reported. Torque consistency comes from replacing the hand driver with the machine’s electric screwdriver and a programmed fastening cycle, so the screw is driven to a setting rather than to a feel.
Cycle time comes from the station layout. With dual fixtures the head never waits for a cabinet to be loaded: the operator assembles the next cabinet at Station 1 and removes the finished one at Station 3 while Station 2 fastens.
| Item | Model | Qty |
|---|---|---|
| LED display cabinet screw fastening machine | JHIMS BL18 (vertical 4-axis) | 1 |
One JHIMS BL18 vertical four-axis screw fastening machine was delivered for LED display cabinet assembly, configured for M4×10 screws and the customer’s cabinet fixtures.
| Feature | Details |
|---|---|
| Screw Specification | M4×10 with flat & spring washers |
| Feeding Method | Feeder pneumatic blowing |
| Number of Axes | 3 fastening axes + 1 feed axis |
| Positioning Accuracy | ±0.02mm |
| Fastening Method | Single-head suction-type fastening |
| Alignment Method | Camera-assisted alignment |
| Max. Compatible Fixture | 1024×1024×105mm |
| Overall Dimensions (L×W×H) | 4700×1800×1500mm |
| Weight | Approx. 550kg |
| Control Method | Motion control card + teach pendant |
| Power Supply | AC 220V, 50Hz |
| Operating Air Pressure | 0.55–0.65MPa |

The axis arrangement is what makes the cabinet the unit of work rather than the module. Three fastening axes position the head over the cabinet and one feed axis brings the screw to the nozzle, so a single machine covers the whole cabinet footprint up to 1024×1024×105mm.
Component selection follows the rest of the JHIMS range: pneumatic cylinders for the clamping and feed axes, a ground ball screw and a linear guide for the axes, servo motors and an electric screwdriver for fastening, with an industrial touch screen on a motion-control-card platform.
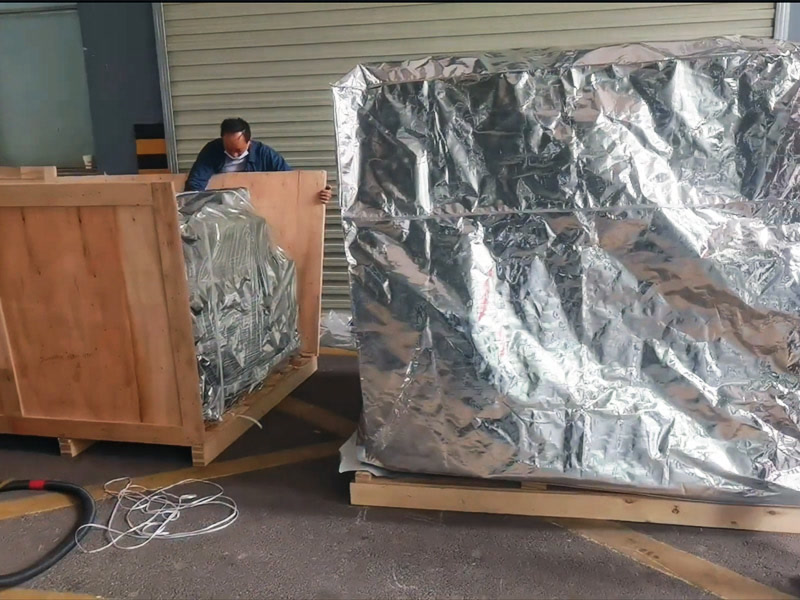
The machine was built with the customer’s cabinet fixtures, and positions were taught with camera-save teaching so the fastening pattern is stored in the machine’s own coordinate system. It was packed in plywood crates and shipped in August 2026.
On arrival the machine is set on the cabinet shop floor, clamped to the existing fixtures and commissioned against the customer’s own cabinets. Operators are trained on program recall, screw-spec change and routine maintenance, because a machine that needs a specialist for every change returns the process to manual speed.
This order did not travel as a finished machine on one frame. The customer’s transport and building access could not take the assembled size, so the BL18 shipped as modules and was assembled on site from the manual, in a production room on the second floor.
That is also why the delivery conversation covered calibration and configuration manuals, online remote support for commissioning, and what ships with the machine versus what the customer supplies locally — including the compressed air, published here as 0.55–0.65MPa so the shop’s supply can be checked before the crates are opened.
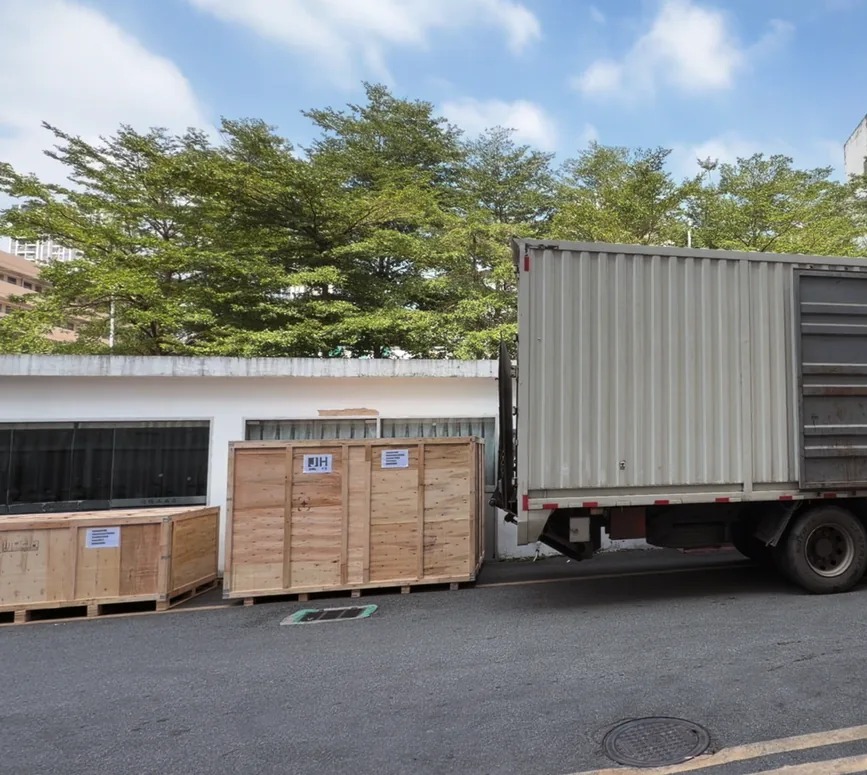

Case studies are easy to write and hard to believe. These are the records from this order: the requirements the customer wrote before shipment, and the loading clips they were sent on the day the crates left Shenzhen.
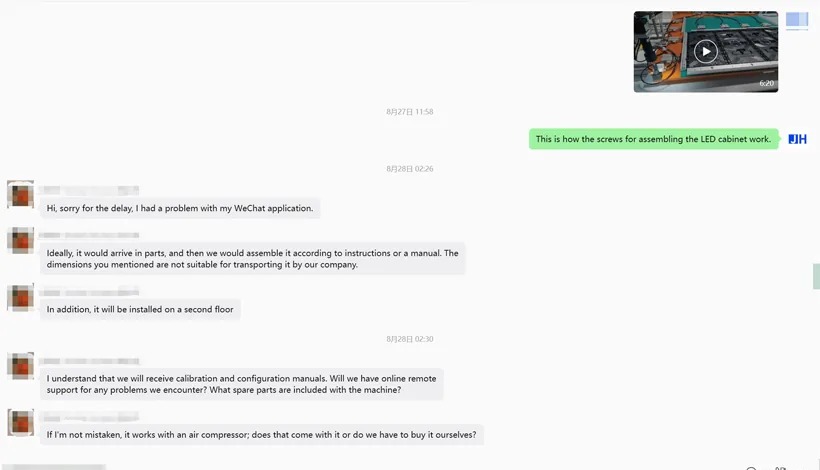
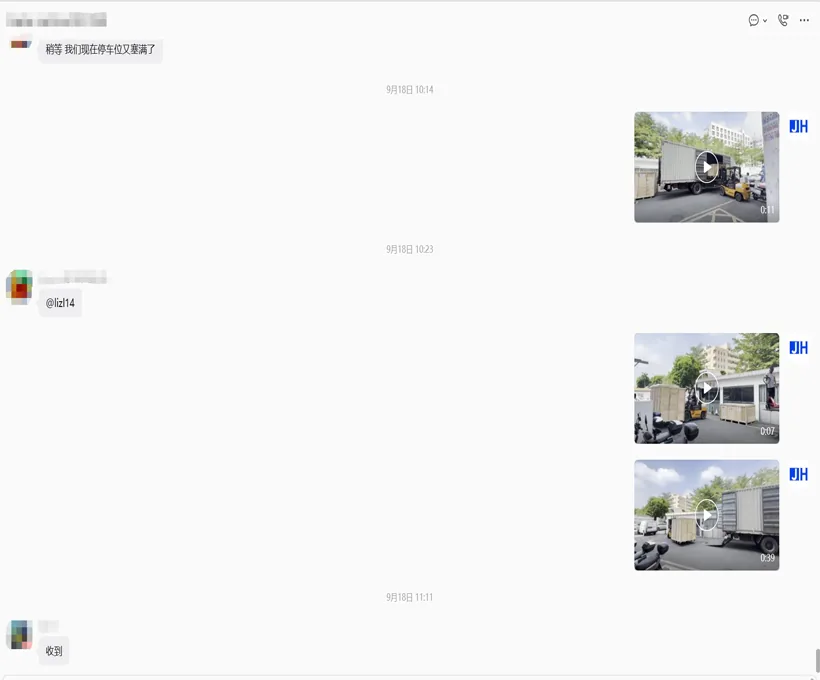
The crates were loaded in Shenzhen on the shipment date, and the customer was sent footage of it as it happened — not a photo staged afterwards.
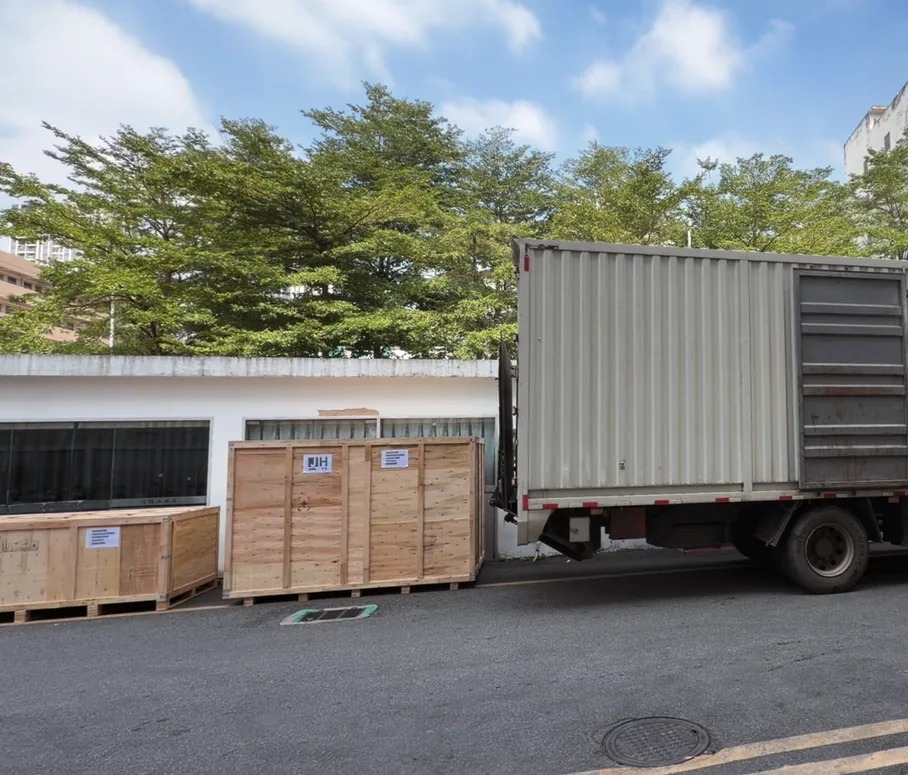
The first clip is the shipment footage from this order; the rest show the BL18 fastening LED display cabinets — module assembly, cabinet handling and automatic screw driving. JHIMS also publishes a 19-part operation series (torque setup, camera calibration, nozzle adjustment, feeder troubleshooting), linked from the JHIMS YouTube channel. The full operator course — all 19 procedures written out, with a fault table — is on the BL18 video guide.
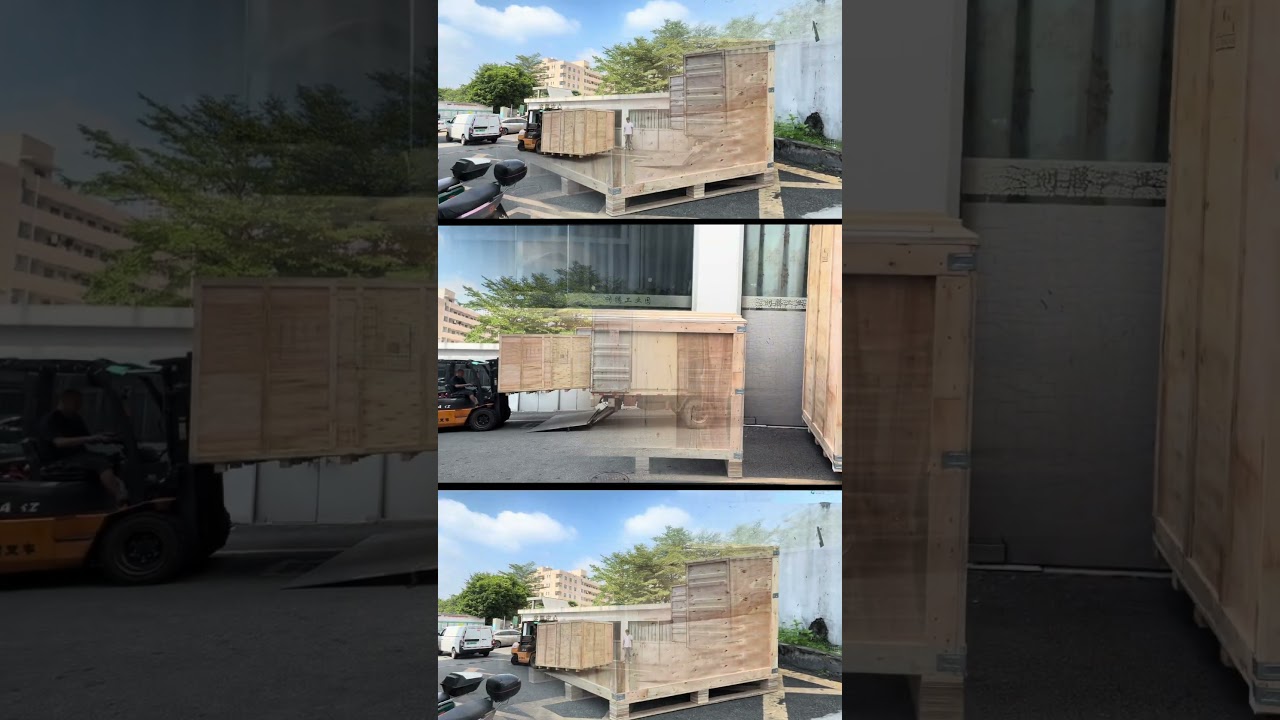
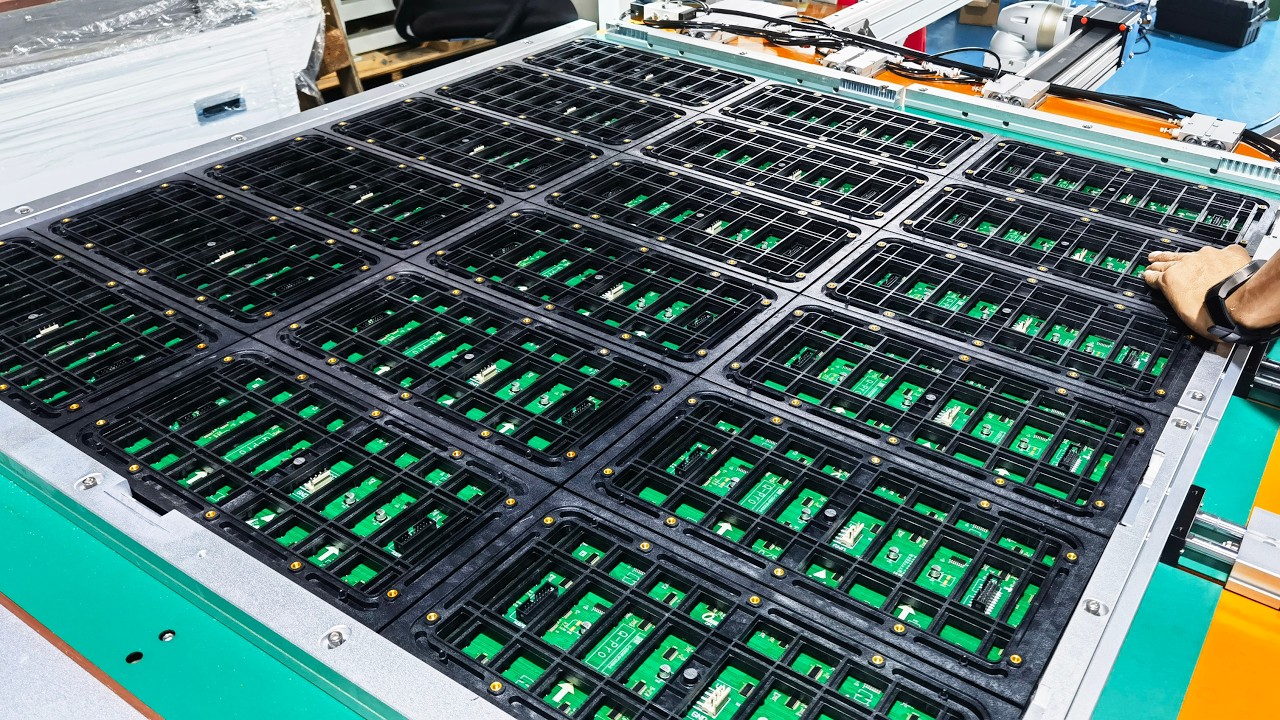
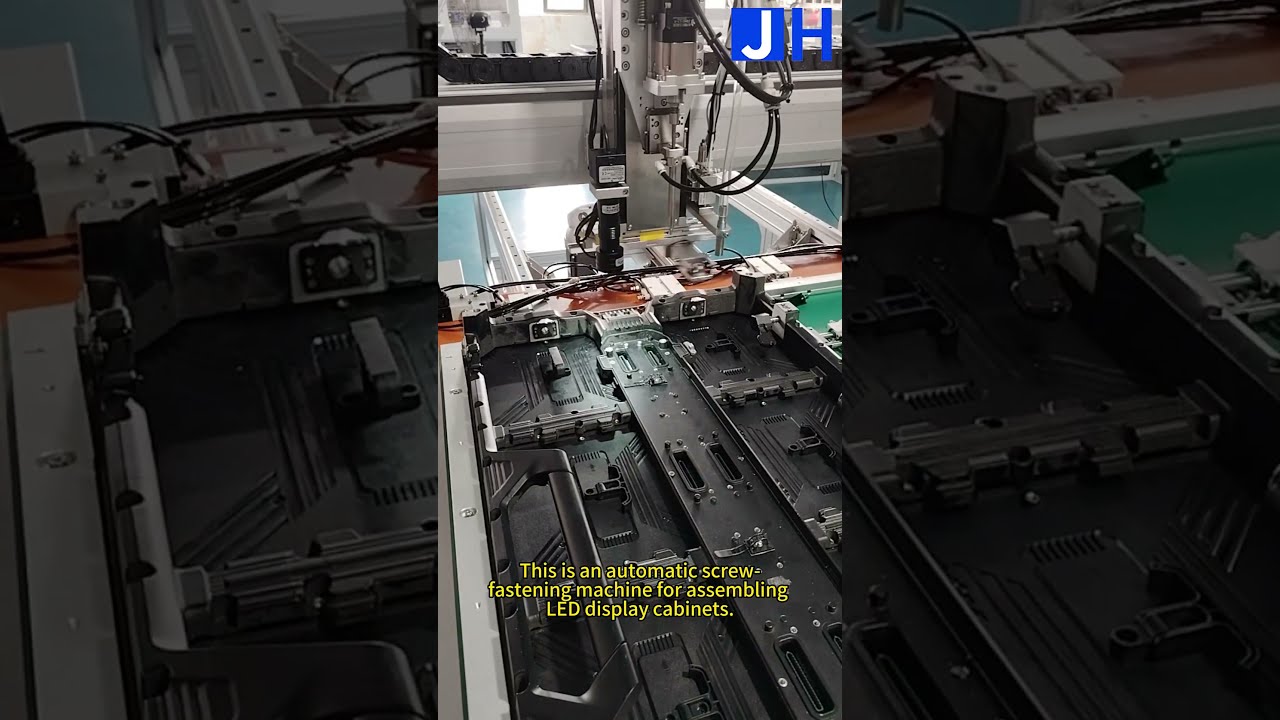
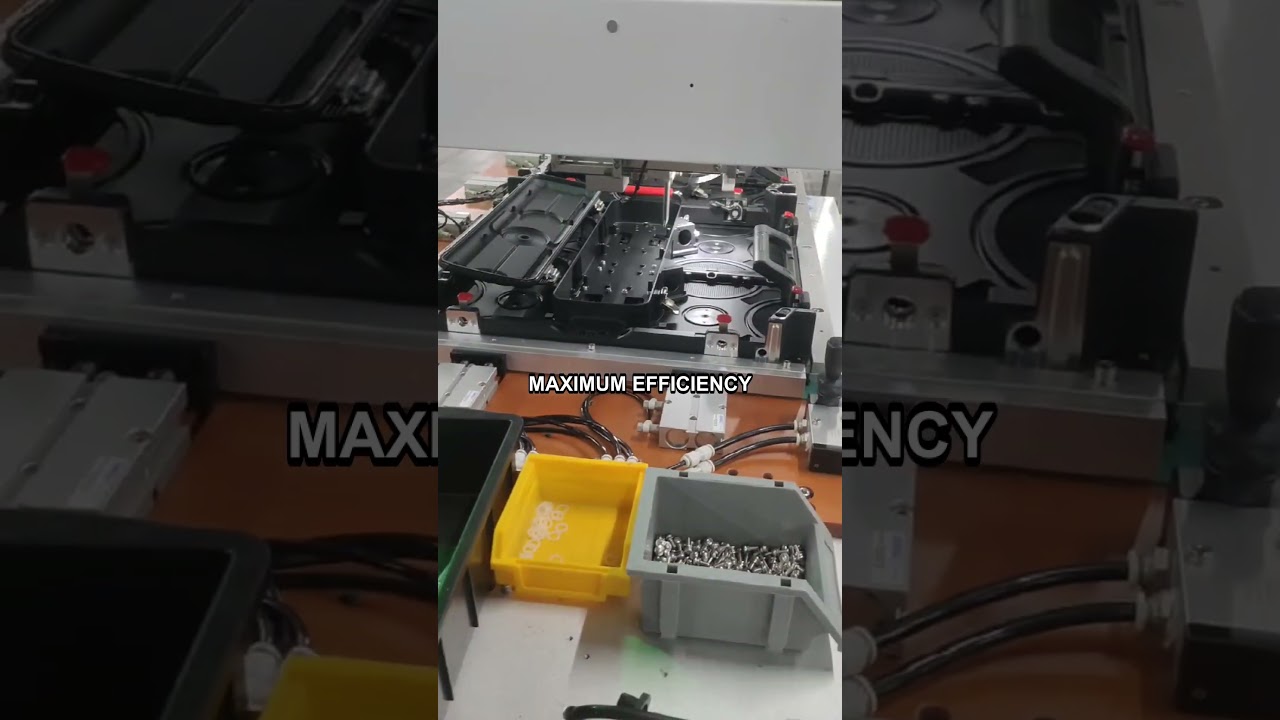
Two things are worth watching for, because they are what separates a machine that demonstrates well from one that holds a cabinet shop’s output: the screw feed should arrive without hesitation or double-picks, and the cabinet should be held flat enough that torque goes into the thread rather than into flexing the panel.
The customer’s own summary is the one that matters here: product quality improved and processing efficiency increased. Both follow from the same change — the fastener no longer receives its torque from a hand.
Quality improved because torque is now a setting rather than a technique. Every screw on every cabinet is driven to the same programmed value, so a cabinet that closes cleanly at the first station closes the same way in the last cabinet of the shift.
Efficiency improved because the operator stopped being part of the fastening cycle. With dual fixtures and three stations, one cabinet is fastened at Station 2 while the next is assembled at Station 1 and the finished one is removed at Station 3, so the head keeps working instead of waiting for a cabinet to be loaded.
The customer’s reported pace is the number worth quoting: about 2.5 seconds per screw. On a single fastening head that works out to roughly 1,440 screws per hour (3,600 ÷ 2.5), and the operator is loading the next cabinet while it happens.
| Measure | Value | Source |
|---|---|---|
| Fastening pace | About 2.5 seconds per screw | Customer-reported |
| Throughput at that pace | About 1,440 screws per hour (3,600 ÷ 2.5) | Calculated from the reported pace |
| Positioning accuracy | ±0.02mm | Machine specification |
| Standard lead time | 30 days | JHIMS delivery |
| Fastening consistency | Machine-applied torque per screw | Machine specification |
What is not published: a rejection rate. The customer’s reported outcome is the pace, the quality and the efficiency improvement; measured per-cabinet defect figures stay with the customer.
Hand tightening looks adequate on a single cabinet and stops being adequate at volume. The M4 fastener is small enough that the difference between a correctly seated screw and one that is over-driven is a narrow torque window, and a hand driver gives no reading of where in that window the screw ended up.
The variation is not usually visible on the finished cabinet. It shows later as a joint that loosens, a panel that creaks under load, or a surface that has been deformed by a driver bit that slipped — which is why manual fastening tends to produce defects that are found at final inspection rather than at the station where they were made.
Automating the step changes what is being controlled. Position comes from the machine’s coordinate system and the taught pattern, torque comes from the electric screwdriver setting, and the sequence comes from the program — three things an operator no longer has to hold in their hands at the same time.
That is also why the fixture matters as much as the head. If the cabinet is not held flat and firm, torque goes into flexing the panel instead of into the thread, and the result is the same inconsistency the machine was bought to remove. Pneumatic clamping on a full-size fixture is part of the solution, not an accessory to it.
The configuration delivered for this project.
| Parameter | Specification |
|---|---|
| Machine | JHIMS BL18 vertical four-axis screw fastening machine |
| Fastening axes | 3 fastening axes + 1 feed axis |
| Screw | M4×10 with flat and spring washers |
| Feeding | Pneumatic blowing, feeder travelling on the X-axis |
| Positioning accuracy | ±0.02mm |
| Alignment | Camera-assisted |
| Max. fixture | 1024×1024×105mm |
| Program storage | 1,000 programs |
| Stations | Three stations, dual fixtures |
| Power / air | AC 220V 50Hz / 0.55–0.65MPa |
| Customer outcome (as reported) | Improved product quality and higher processing efficiency |
FeaturedBL18 Vertical 4-Axis Screw MachineVertical 4-axis cabinet fastening — ±0.02mm, M4×10, fixtures up to 1024×1024×105mm, 1,000 programs.View product → CompanionZM320 Desktop Screw MachineFour-axis desktop screw fastening with air-blowing feed for smaller LED boards and modules.View product →
 UpstreamR10 Reflow OvenLead-free reflow soldering upstream of cabinet assembly for LED circuit boards.View product →
 UpstreamDPS-2 Lens Vibratory FeederVibratory lens feeding for LED module lines — 3–25mm lenses at 0.5–1s per lens.View product →CategoryScrew Fastening SystemsDesktop, handheld and vacuum-pick screw driving machines for electronics assembly.View product →
 Case StudyScrew Tightening: Saudi ArabiaA JHIMS screw tightening machine automating LED display cabinet assembly in Saudi Arabia.Read article →
 Case StudyLED Manufacturing: SpainFour used YSM20R machines for a Spanish LED display manufacturer.Read article →
 Case StudyLens Feeder: DongguanCustom lens feeder built for a Dongguan LED assembly line.Read article →
 SupportTechnical SupportRemote diagnostics, spare parts and service requests for JHIMS machines.Read article →
Send us your cabinet size, screw specification and target output — JHIMS engineering replies within 12 working hours (Mon–Sat, 09:00–23:00 China Standard Time, UTC+8).















